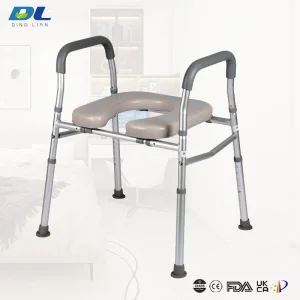
 Dinglian Dl-2016la Bariatric Toilet Safety Frame for Wide Users Medical Commode Handrail for Safety
 Dinglian Dl-2016la Sturdy Toilet Safety Frame with Grab Bars Bariatric Disabled Toilet Aid for Support
 Dinglian Dl-2016la Heavy Duty Toilet Safety Frame with Grab Bars Bariatric Commode Handrail for Disabled Users
 Dinglian Dl-2016la Bariatric Commode Handrail with High-Capacity Durable Toilet Safety Frame for Disabled Users
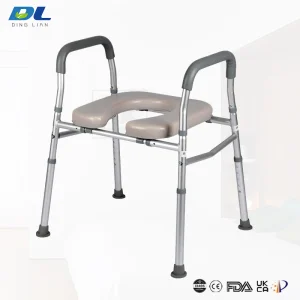 Dinglian Dl-2016la High Strength Commode Handrail for Bariatric Patients Heavy Duty Toilet Grab Bars
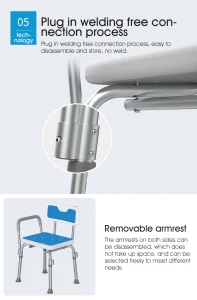 Sturdy Adjustable Shower Bench Chair for Bariatric Support
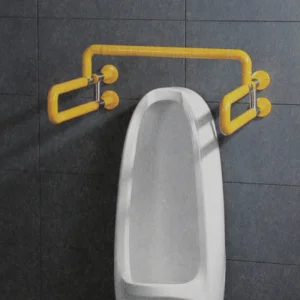 Bathroom Support for Elderly Bariatric Disabled Handicap Rails Grab Bars Toilet Rail
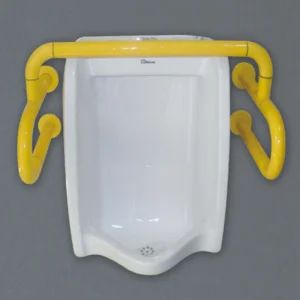 Bathroom Support for Elderly Bariatric Disabled Handicap Rails Urinal Grab Bars Toilet Rail
Analyzing the shift towards specialized high-capacity medical equipment in the 21st century.
The global bariatric equipment market is witnessing unprecedented growth, projected to expand at a CAGR of 6.5% over the next decade. As obesity rates rise globally—notably in North America, the Middle East, and parts of Europe—the demand for Heavy-Duty Bariatric Safety Rails has transitioned from a niche requirement to a standard industrial necessity. Hospitals and long-term care facilities are now mandated by safety regulations to install rails capable of supporting up to 600lbs (272kg) or more.
Modern bariatric safety rails are no longer just "larger versions" of standard rails. The trend is moving toward Intelligent Design: antimicrobial coatings, ergonomic "soft-grip" surfaces, and modular installations that do not require invasive wall reinforcement. Innovations such as Floor-to-Ceiling tension rails and Folding lateral supports are becoming preferred choices for versatile room configurations in AI-integrated smart hospitals.
International medical procurement officers are increasingly prioritizing three factors: Certified Load-Bearing Ratings, Material Longevity (Stainless Steel 304 or High-Density ABS Nylon), and Supply Chain Reliability. Large-scale public health tenders in the UK, USA, and Germany are seeking manufacturing partners who can provide comprehensive data on stress testing and corrosion resistance, moving away from low-cost, unverified alternatives.
21 Years of Excellence in Medical Technology Innovation
Founded in 2003, Shenzhen Avelar Medical Co., Ltd. has established itself as a cornerstone in the global medical technology industry. With a massive 10,000 square meter production facility across Huizhou and Pingshan, we represent the pinnacle of National High-Tech Enterprise excellence.
Our commitment to the E-E-A-T principles is reflected in our robust R&D infrastructure. We don't just manufacture; we innovate. Our team of 100+ engineers works tirelessly to ensure that every Bariatric Toilet Safety Frame and Medical Commode Handrail exceeds international safety benchmarks.

Tailored solutions for diverse architectural and clinical environments.
High-traffic ERs and ICU bathrooms require wall-mounted stainless steel railings that can withstand constant chemical sterilization and extreme physical force. Our Commercial-Grade Patient Handling machines complement these rails for seamless transfers.
Senior living centers prioritize comfort and "home-like" aesthetics. Our ABS Nylon Grab Bars offer a warm-to-touch surface and varied colors (Yellow/White) to assist patients with visual impairments while maintaining a non-clinical atmosphere.
For home use, space-saving is key. Our Folding Shower Chairs and Adjustable Toilet Frames allow family members to use the same space without obstruction, providing safety only when needed.
The China Advantage: Quality, Scale, and Customization.
Utilizing 200+ advanced manufacturing units, including robotic welding and CNC precision cutters, we ensure that every joint in our bariatric rails is failure-proof.
As a direct manufacturer, we offer full customization. Whether you need specific dimensions for a bariatric ward or custom branding for your medical supply chain, we deliver.
Our business philosophy of "Quality First" ensures every product shipped meets ISO and CE standards, providing the reliability required for global healthcare tenders.
 Wall Mounted ABS Nylon Grab Bar Bathroom Safety Rail for Handicap and Bariatric Support High Strength Material
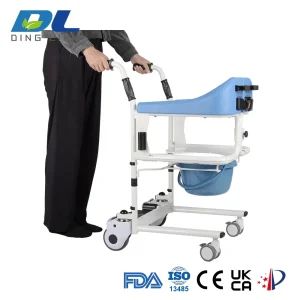 Commercial-Grade Patient Handling Machine - Multi-Function Shifter for Bariatric Transport, Wheelchair & Hygiene Care
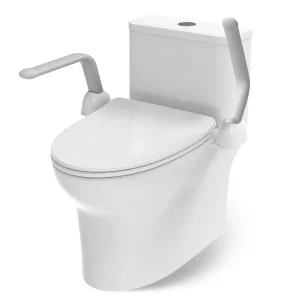 Heinsy Medical Toilet Handrail Railing Helper for Elderly, Handicap, Disabled, Seniors - Bariatric Assist Handrail Grab Bar
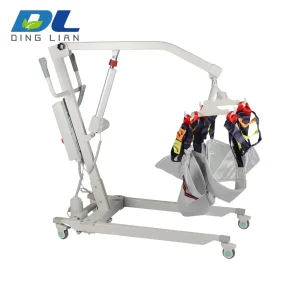 Dl-Wgyw05 Heavy-Duty Electric Shifter for Bariatric Patients - High Weight Capacity & Stable Mobile Base
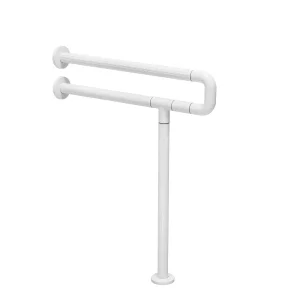 Disabled Elderly Pregnant Medical Safety Support Stainless Steel Toilet Grab Bar
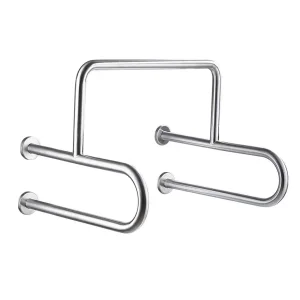 Elderly Handicapped Wall Mounted Bathroom Support Toilet Safety Railing Stainless Steel Handicapped Handrail Railing
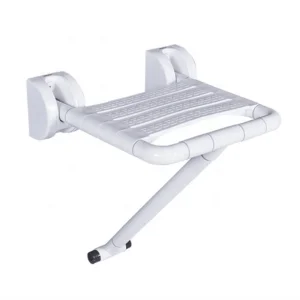 Support Bench Bathroom Bathtub Safety Stool Chair Wall Mounted Folding Shower Chair
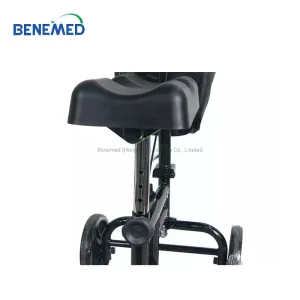 Disabled Scooter with 4 Wheel Knee Support Pad Mobility Scooter Bariatric Products
 Avelar Medical