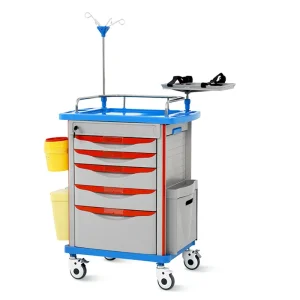
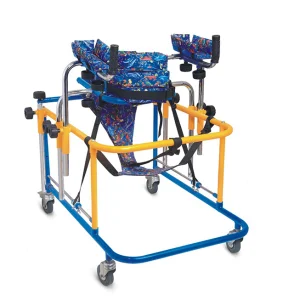
Shenzhen Avelar Medical Co., Ltd. (est. 2003) represents the pinnacle of CE-certified medical manufacturing. As the global healthcare landscape pivots towards aging-in-place and long-term care, our Pingshan-based R&D and Huizhou-based manufacturing facility operate at the intersection of quality and scalability. With over 21 years of expertise, we provide the essential hardware backbone for Chronic Care Management (CCM) programs worldwide.
Why do global enterprises choose Avelar Medical? Beyond our 10,000 square meter state-of-the-art facility, we leverage a deep supply chain integration. From laser cutting to assembly, our in-house control ensures compliance with international standards (CE, ISO). Our "Information Gain" approach to manufacturing means we don't just build products; we optimize them for the clinical environment, reducing the cognitive load on healthcare providers and enhancing patient comfort through ergonomic design.
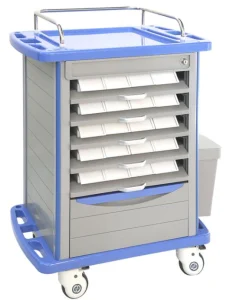
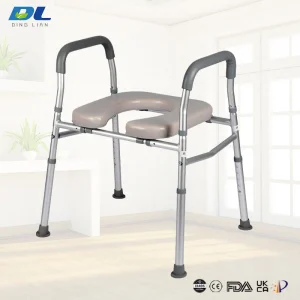
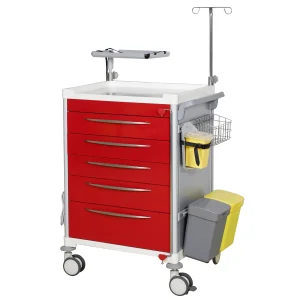
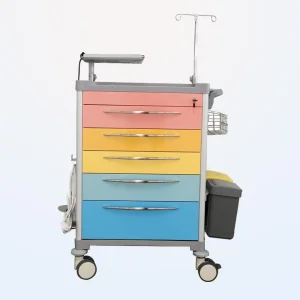
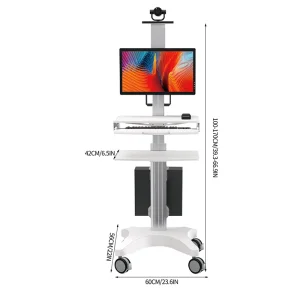
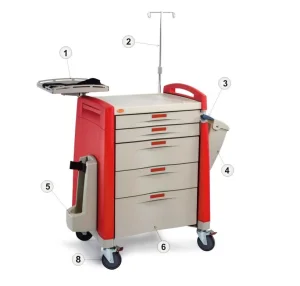
The transition from reactive to predictive care is driving demand for specialized infrastructure. Modern CCM tools now require high mobility, interoperability with telemedicine terminals, and uncompromising durability. Avelar Medical is at the forefront of this shift, producing advanced hospital carts, mobile computer terminals, and patient support systems that adapt to the fast-paced nature of modern surgical and emergency centers.
All Avelar Medical products are manufactured under rigorous quality systems, carrying essential CE certifications and adhering to ISO international standards for medical device manufacturing.
We serve over 100 countries. Our production capability, featuring 200+ advanced manufacturing units, ensures short lead times and consistent batch quality for hospitals and private healthcare institutions worldwide.
 Avelar Medical