Empowering Global Medical Infrastructure with Intelligent Point-of-Care Trolleys, Telemedicine Workstations, Ergonomic IV Infusion Systems & Advanced Clinical Mobility Solutions by Shenzhen Avelar Medical Co., Ltd.
Precision-engineered CE compliant hospital workstations, crash carts, and mobility infrastructure for high-efficiency clinical workflows.
An in-depth evaluation of regulatory compliance, point-of-care workflow optimization, and technical specifications driving hospital hardware procurement worldwide.
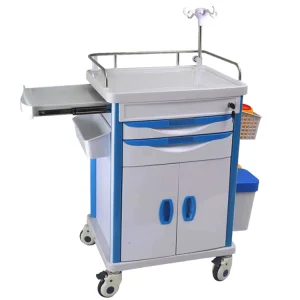
Modern healthcare systems demand frictionless mobility. Integrating mobile all-in-one computer carts and intelligent medication dispensing trolleys reduces nurse walking distances by up to 38%, mitigating burnout and dramatically minimizing point-of-care charting latency in critical care wards.
Navigating EU Medical Device Regulation (MDR 2017/745) requires rigorous mechanical stability, tip-over testing, anti-static electrostatic discharge (ESD) protection, and medical-grade power distribution. Our delivery systems comply fully with IEC 60601-1 structural and electrical standards.
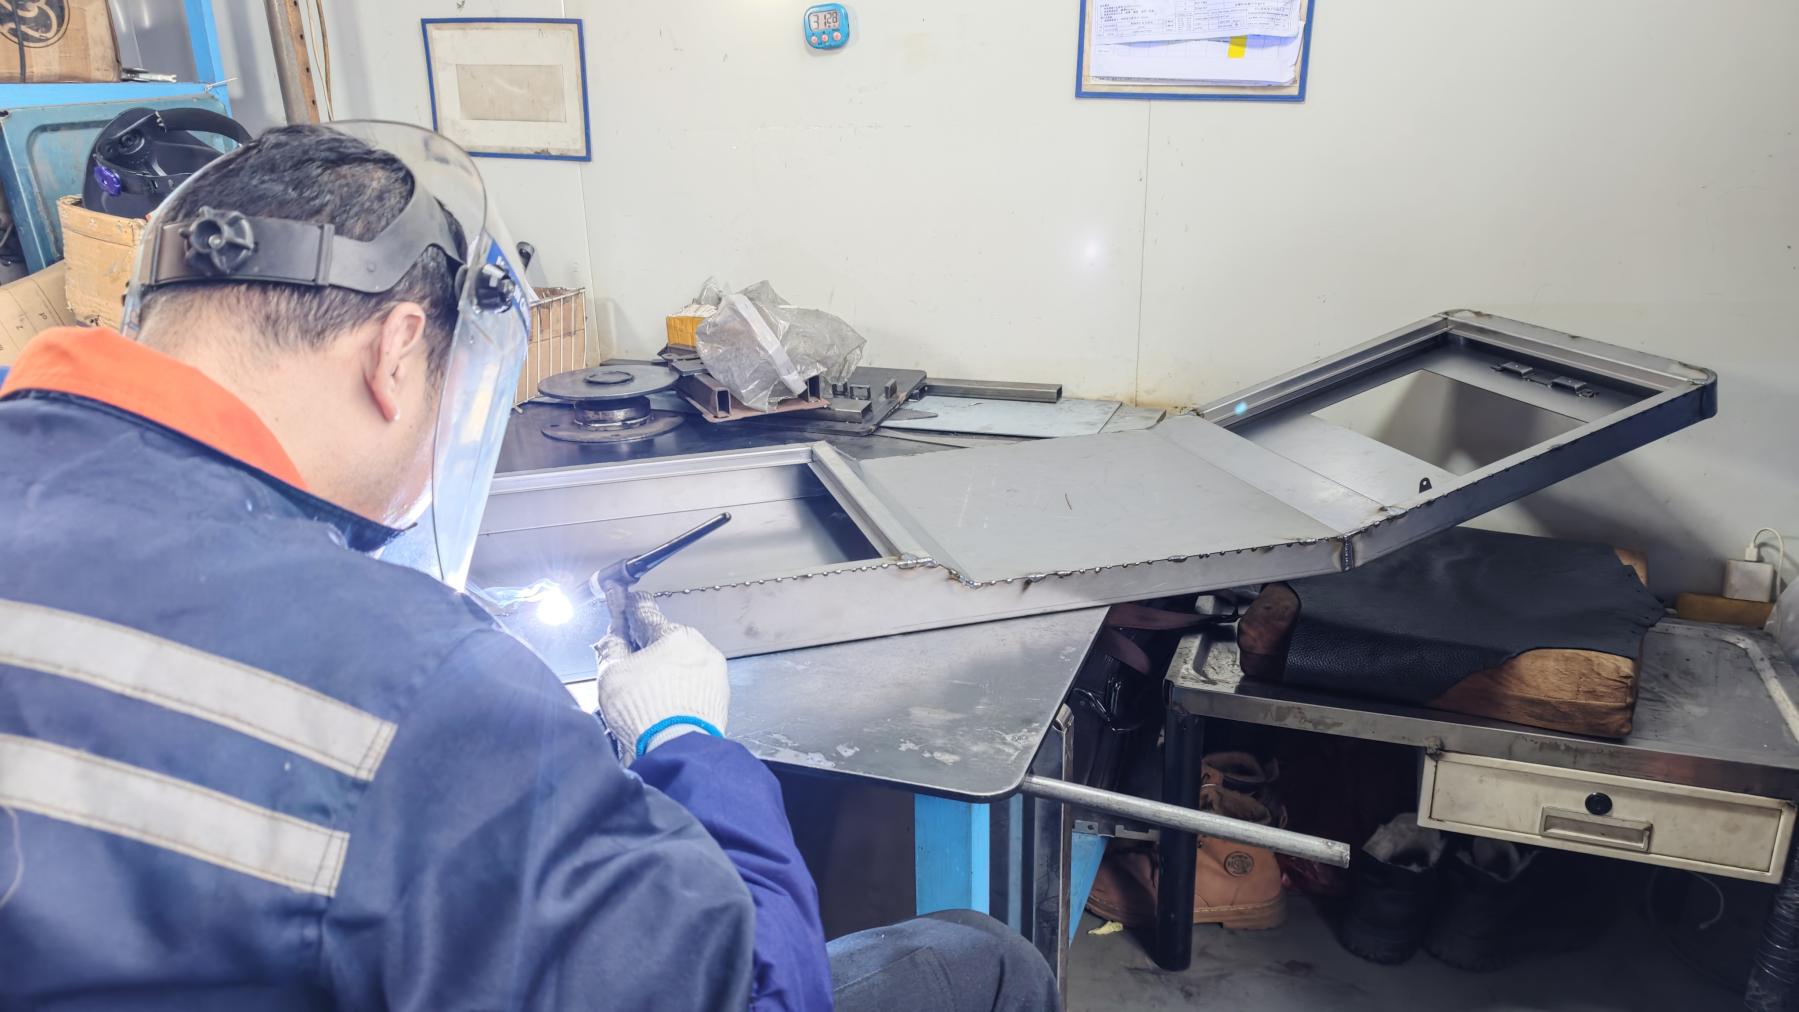
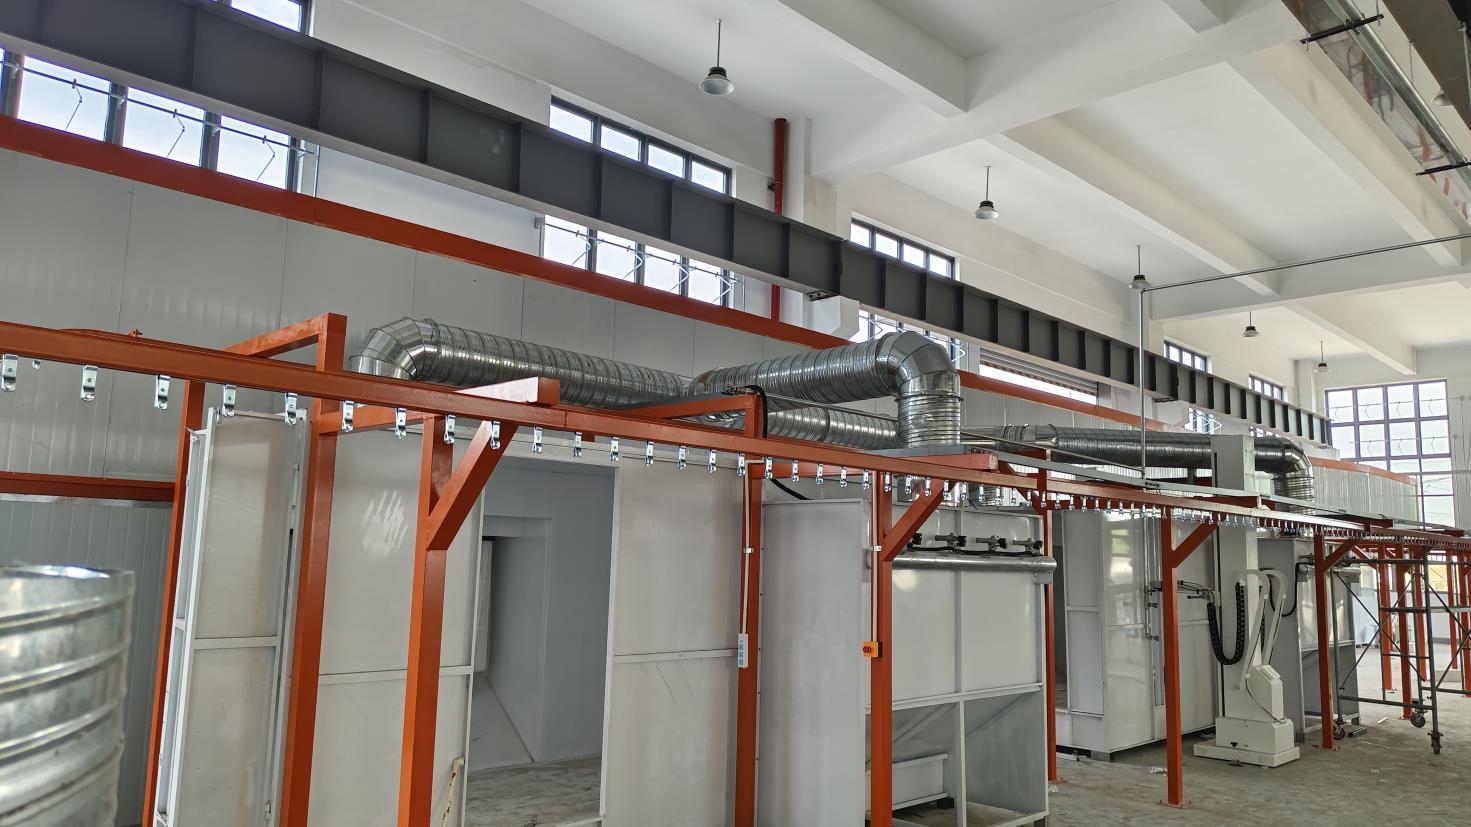
Hospital-acquired infections (HAIs) represent a major global liability. Healthcare delivery carts must endure harsh chemical disinfectants. Avelar Medical utilizes proprietary non-porous antimicrobial powder coatings and seamless stainless steel welds to prevent bacterial colonization.
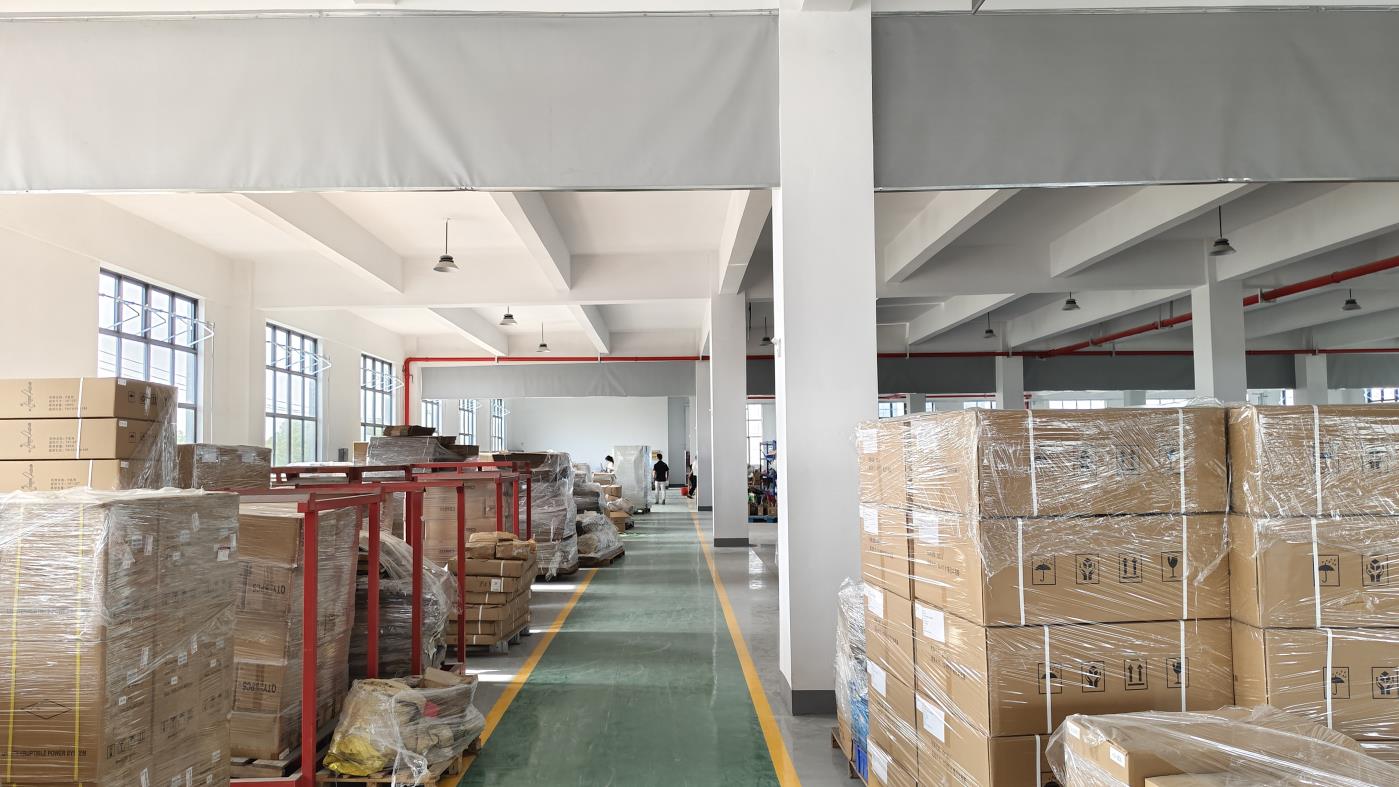
Shenzhen Avelar Medical Co., Ltd. was founded in 2003 and has accumulated over 21 years of rich experience in the medical technology industry. Headquartered in Pingshan, Shenzhen, with a state-of-the-art production facility in Huizhou, the company spans a total area of 10,000 square meters. As a leading national high-tech enterprise, Avelar Medical integrates cutting-edge research and development, innovative design, and high-efficiency manufacturing to deliver superior medical and healthcare solutions.
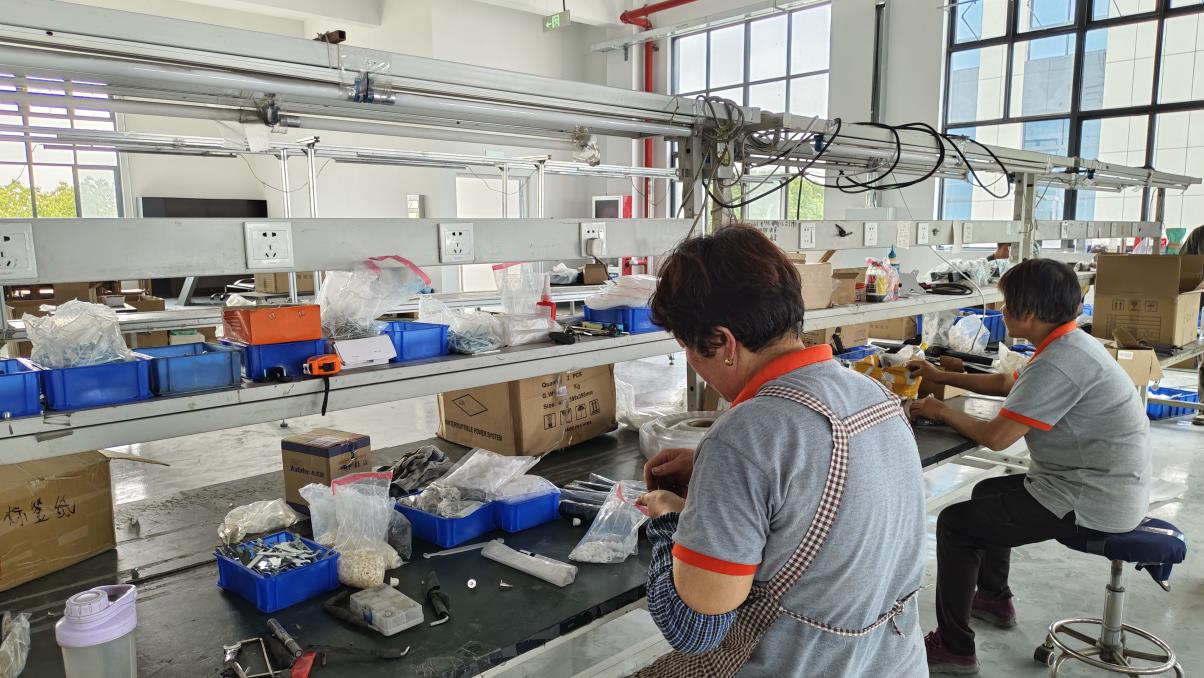
With a team of over 100 highly skilled engineers and technical professionals, and more than 200 advanced manufacturing units, Avelar Medical is committed to pushing the boundaries of technological advancements in the medical field. The company has secured more than 100 national patents, demonstrating our continuous focus on innovation.
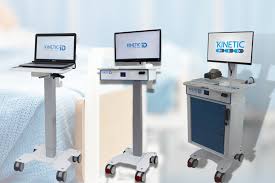
Avelar Medical specializes in a broad range of products, including medical equipment installation solutions, intelligent mobile medical devices, assistive technology for residual life support, healthcare products for the bathroom, and more. We work closely with top-tier hospitals and healthcare institutions around the world, providing them with products designed to improve patient care, enhance operational efficiency, and optimize the healthcare environment. Our solutions have reached more than 100 countries and regions, including North America, Europe, the Middle East, and Asia.
At Shenzhen Avelar Medical, our business philosophy revolves around two core principles: “Quality First” and “Customer First.” This commitment to excellence has earned us the trust of our domestic and international clients. Our innovative products, combined with exceptional service and reliable after-sales support, allow us to meet the ever-evolving needs of the global healthcare market.
As we look to the future, Avelar Medical remains dedicated to continuous growth, investment in research and development, and the creation of cutting-edge medical solutions. We are committed to improving healthcare outcomes, fostering a healthier future for communities worldwide, and making a lasting impact on the global healthcare industry.
Empirical performance metrics reflecting our global medical manufacturing output.
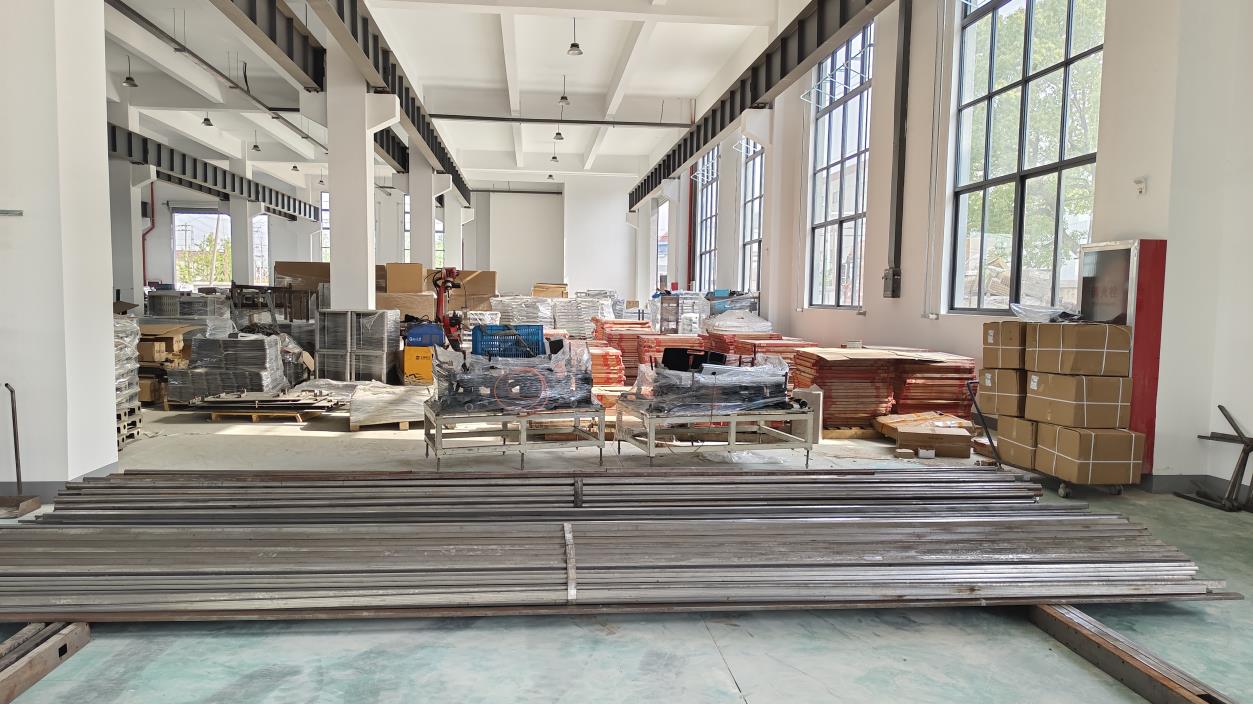
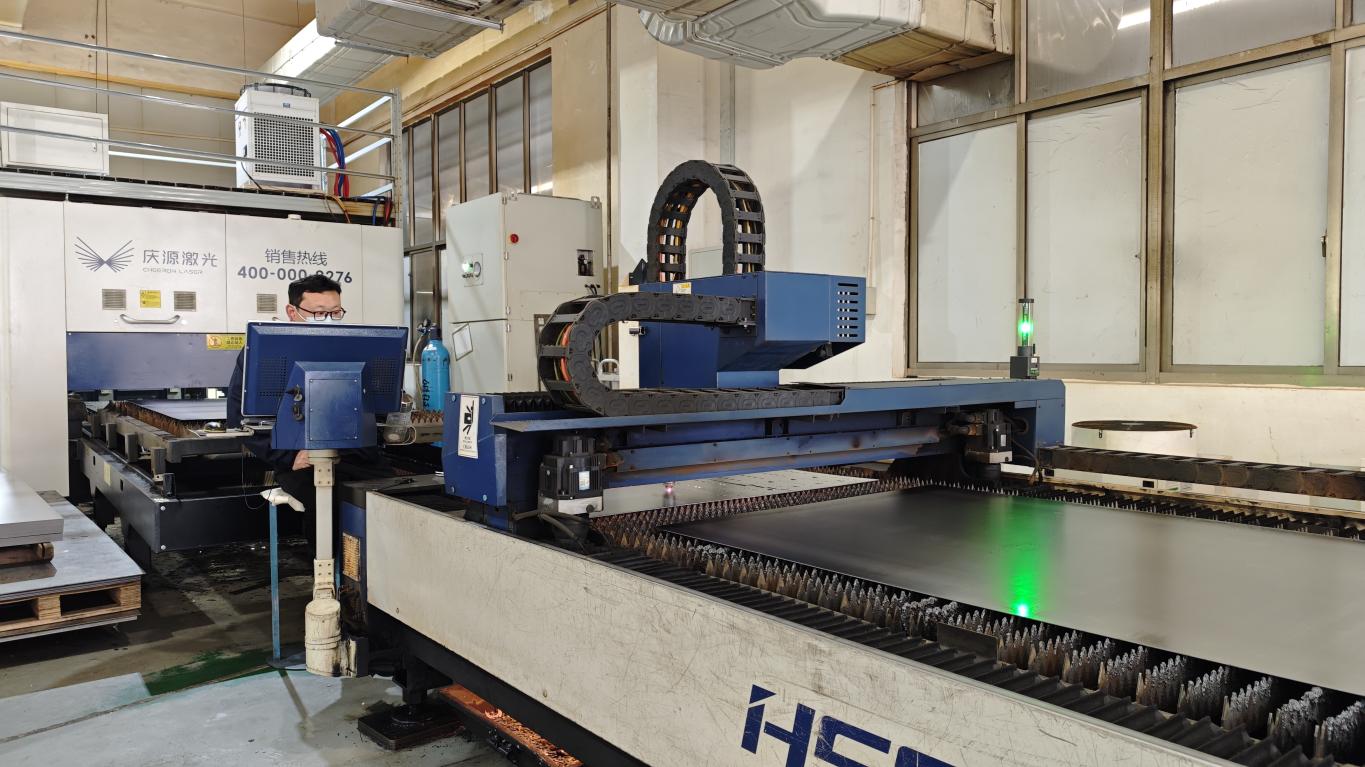
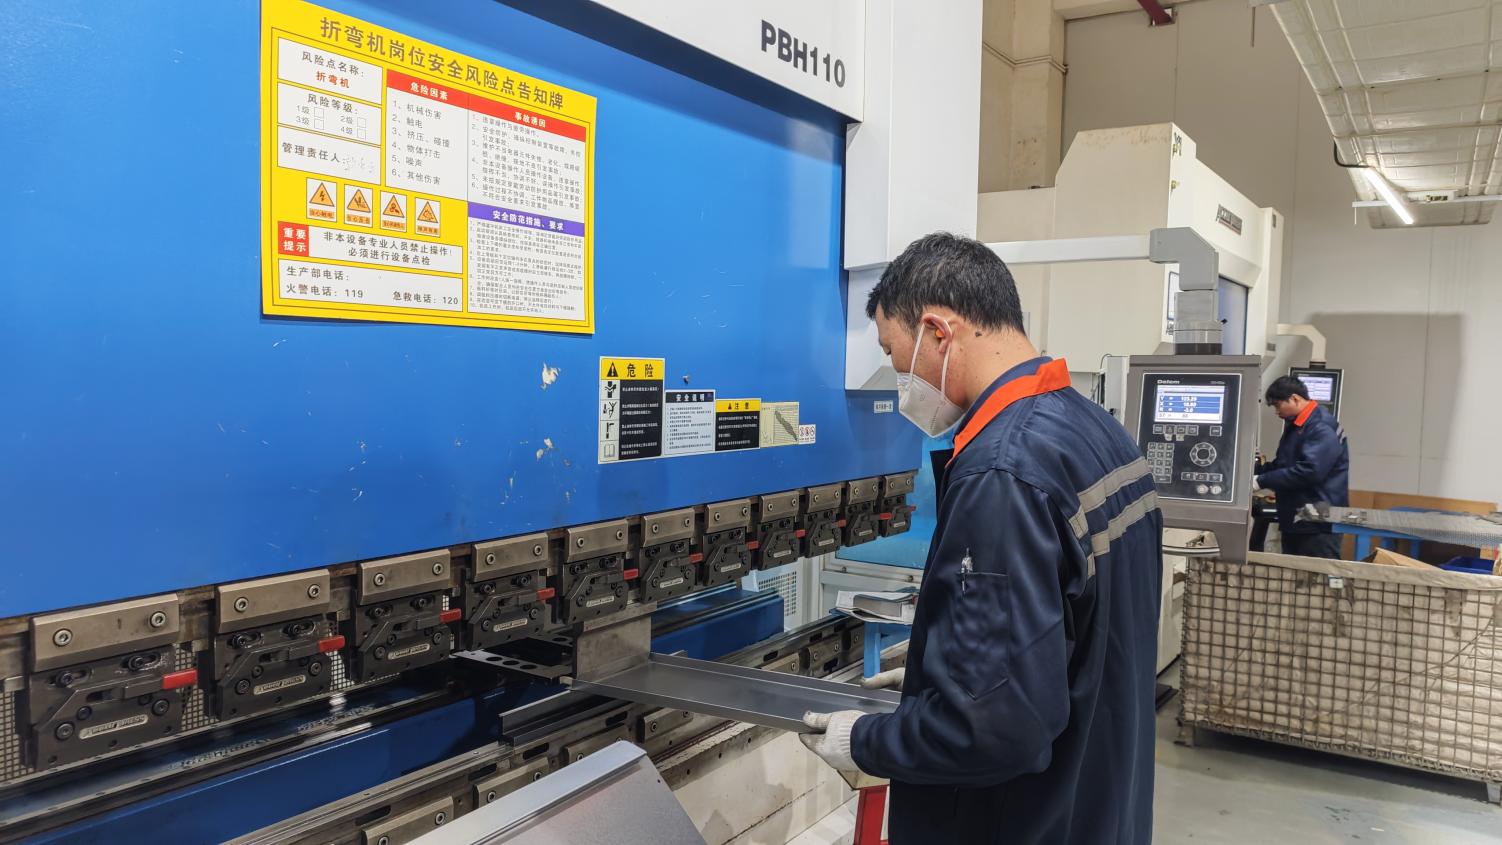
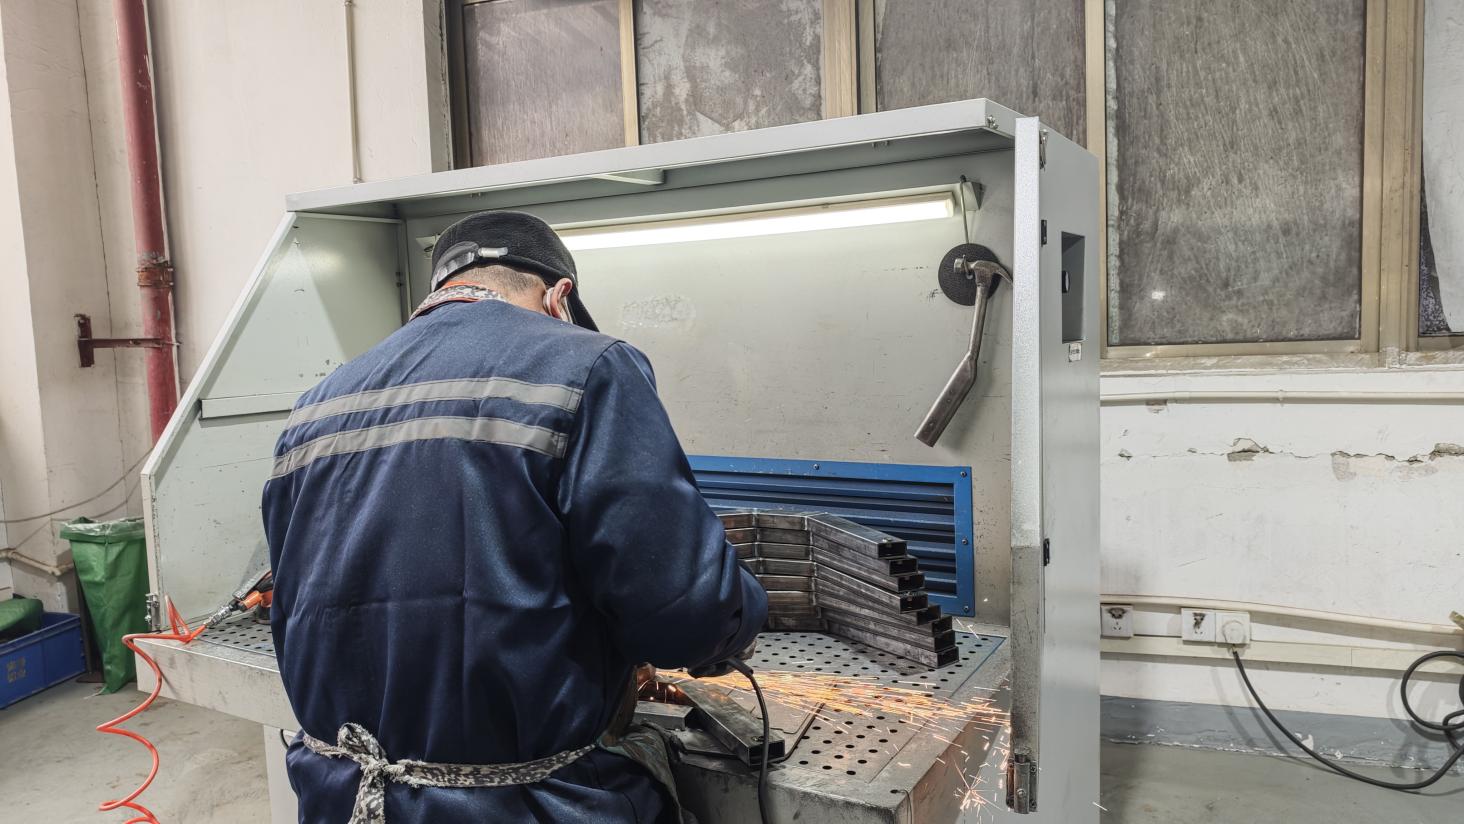
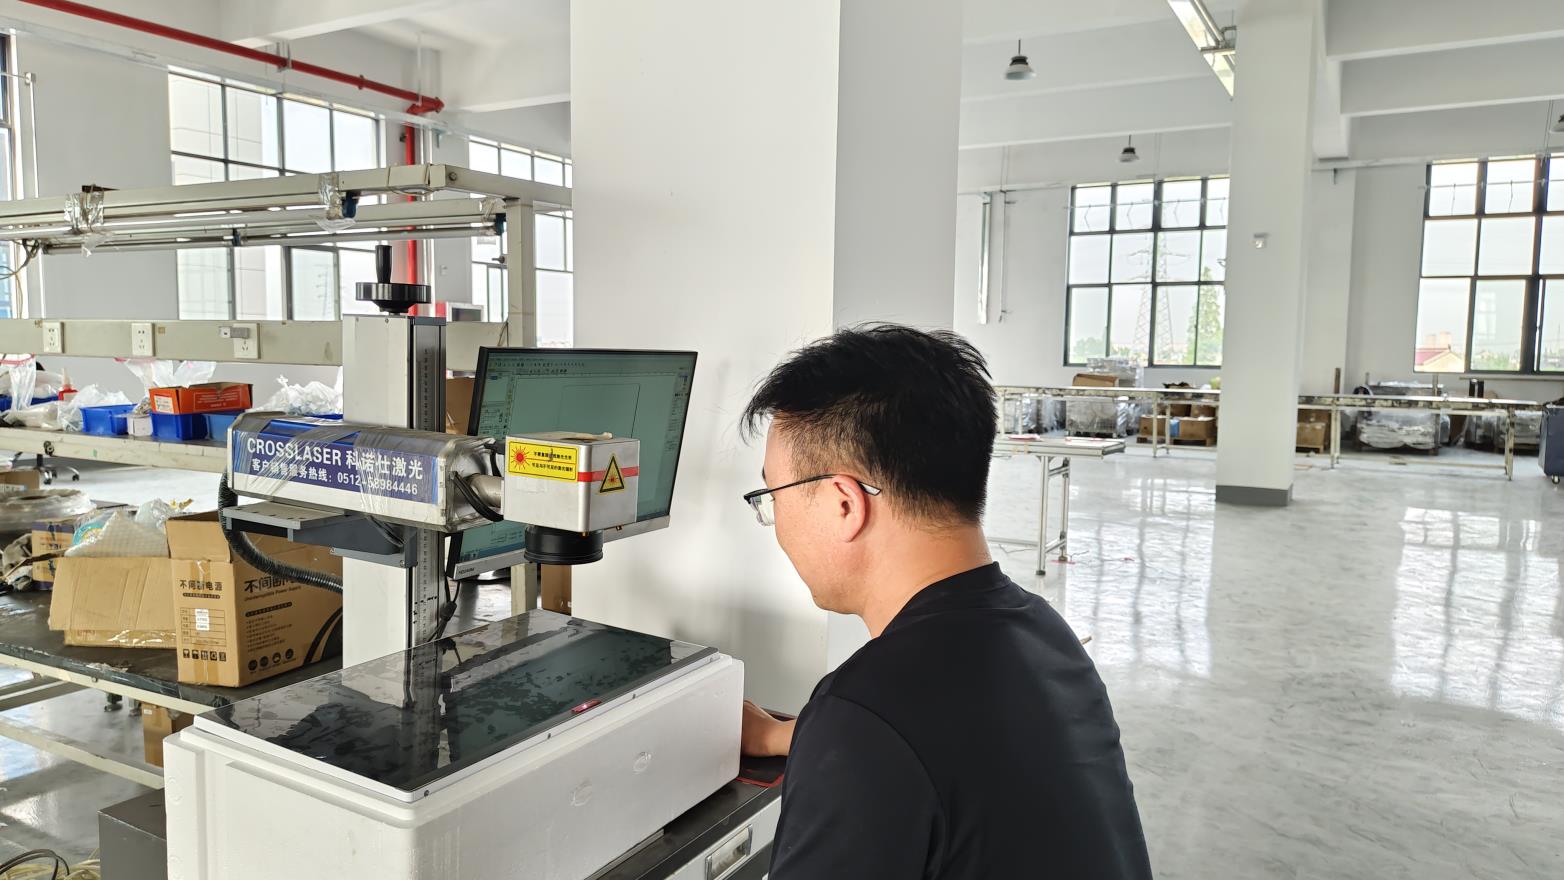
Inside our Huizhou manufacturing hub: Seamless integration of heavy precision machinery, automated sheet metal fabrication, electrostatic surface treatment, and strict quality control.
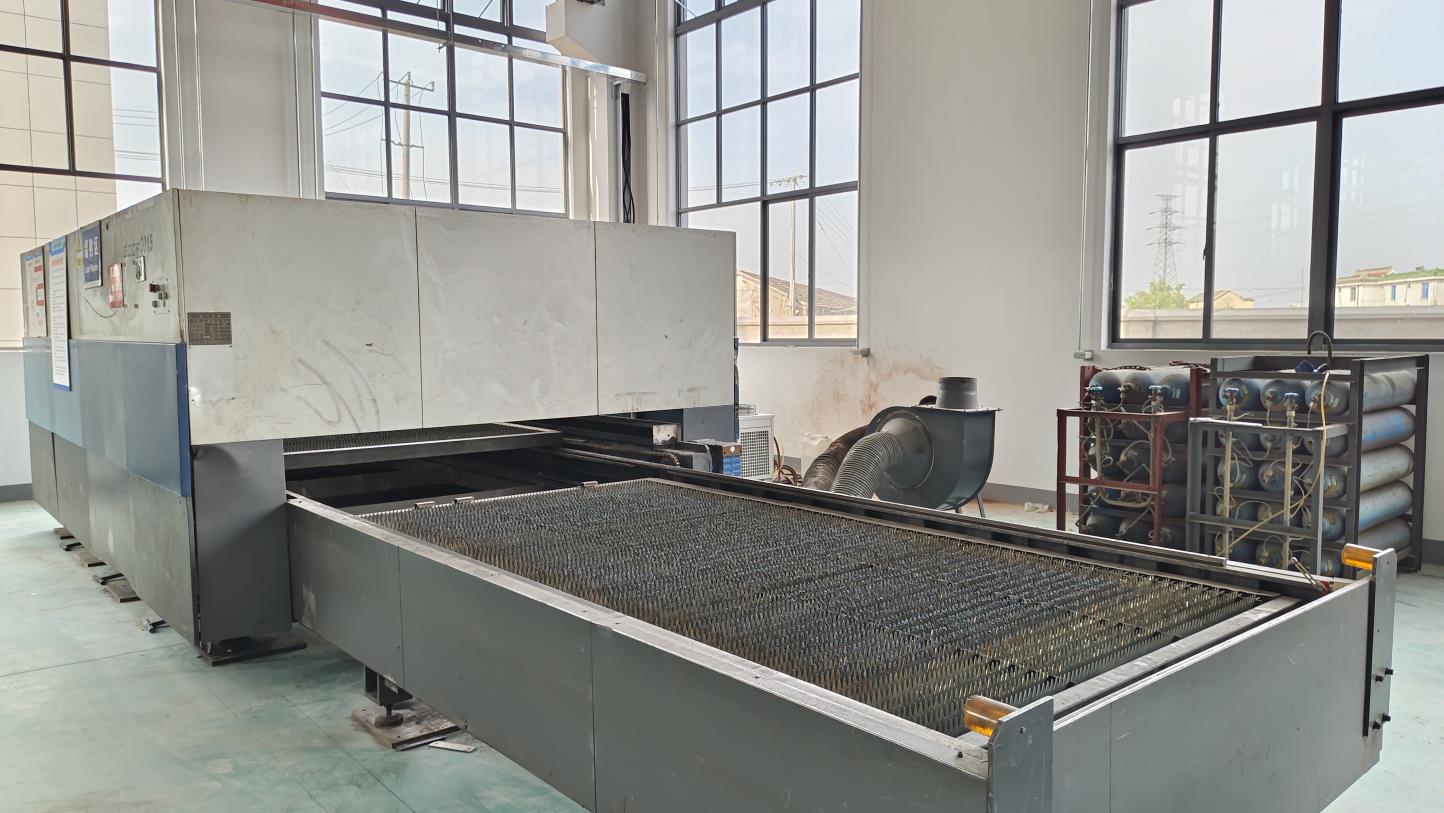
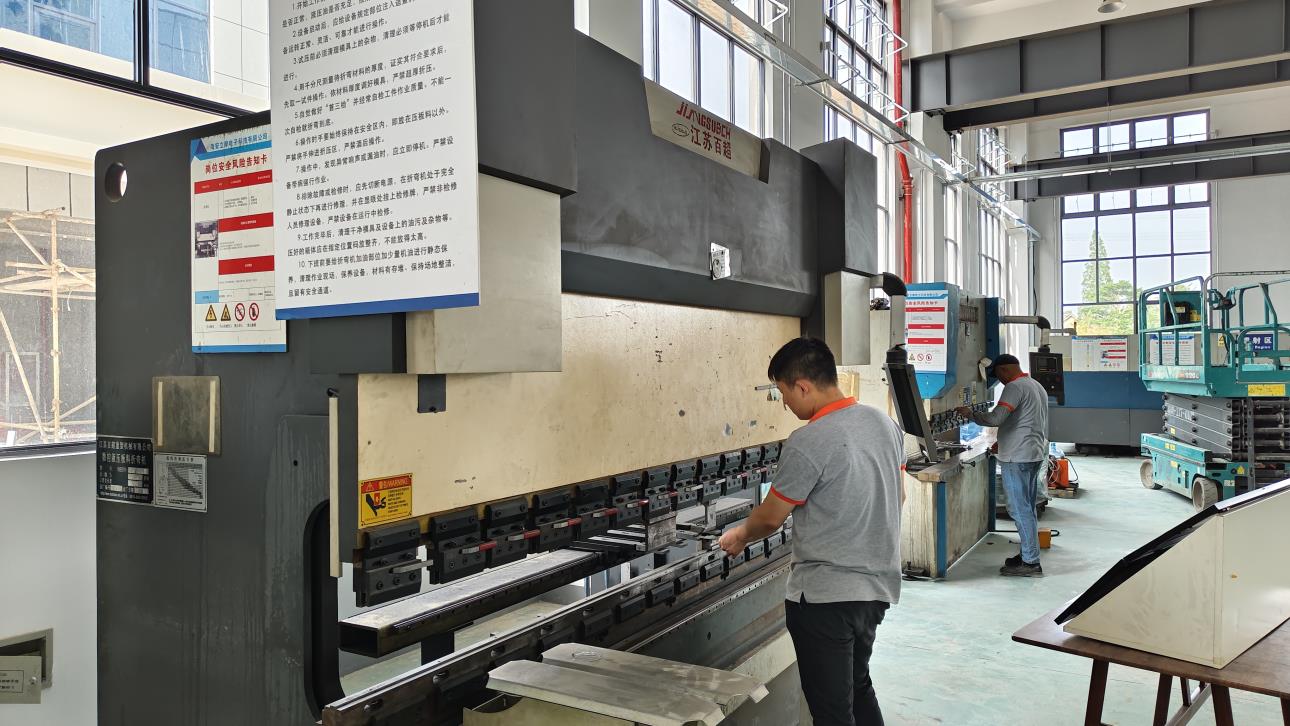
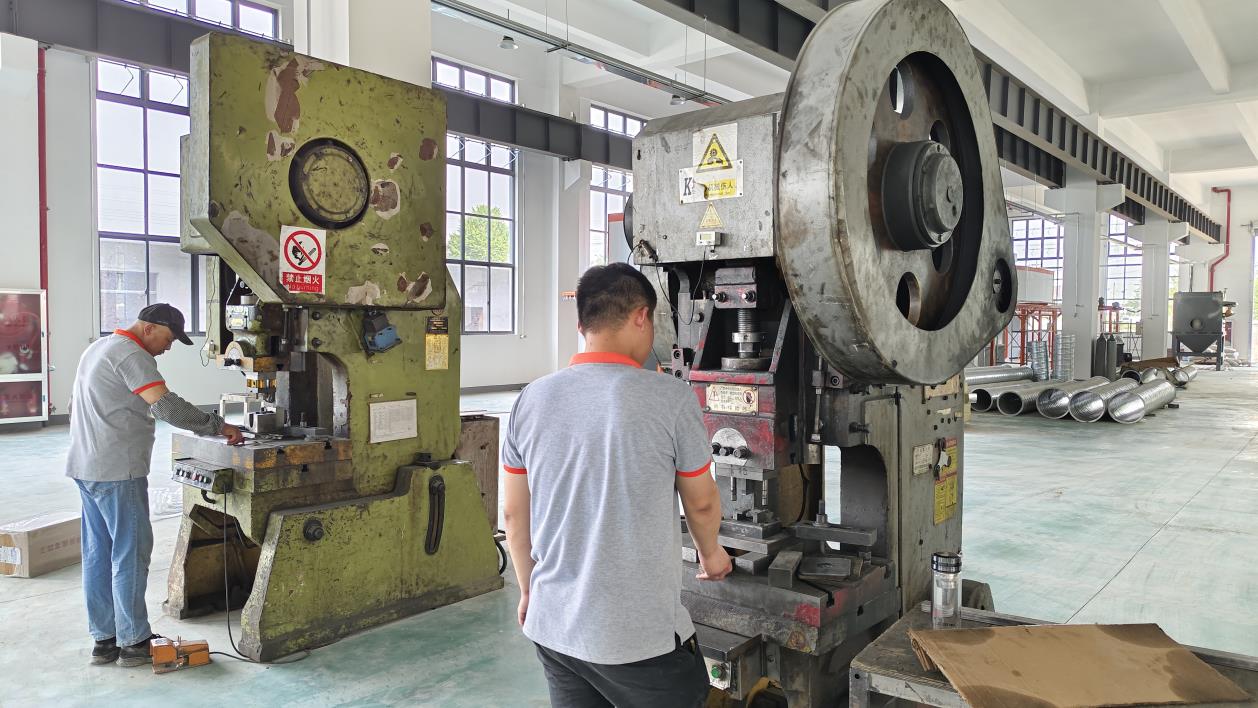
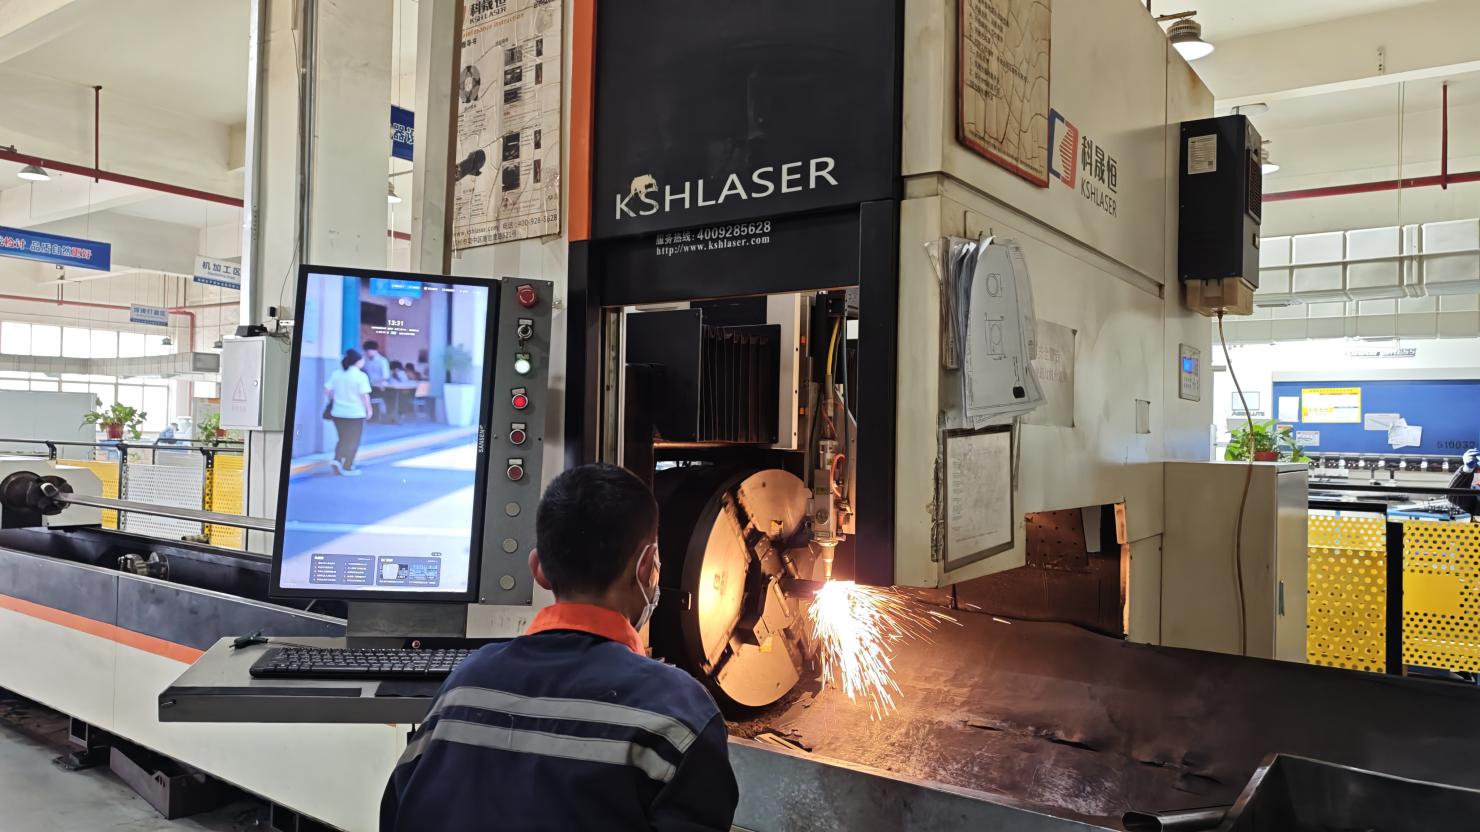
Tailored hospital delivery solutions engineered to satisfy demanding regional regulations, custom OEM specifications, and diverse clinical environments.
Equipped with gas-spring pneumatic height adjustment, integrated dual-monitor VESA mounts, anti-vibration shock absorption, and silent medical-grade casters. Designed for zero-drift performance during delicate surgical interventions.
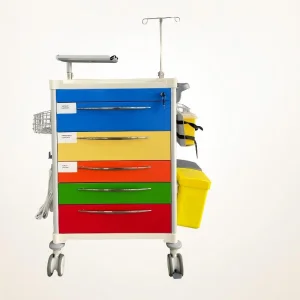
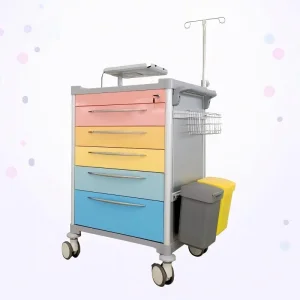
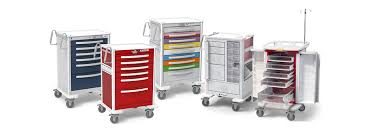
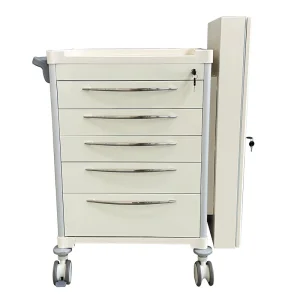
High-strength color-coded emergency crash carts designed for rapid response. Includes breakaway security seals, tilt bins, integrated oxygen tank holders, defibrillator shelves, and CPR board mounts for instant emergency readiness.
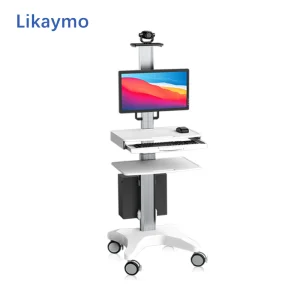
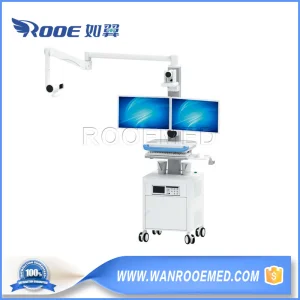
Advanced mobile workstations featuring built-in LiFePO4 battery power supply modules, HD video conferencing camera brackets, micro-PC mounting enclosures, and all-day mobile operational capability for rural and remote specialist consultations.
Anticipating the next decade of biomedical hardware evolution through smart IoT integration and lightweight ergonomic design.
The next generation of clinical emergency trolleys is transitioning from physical keys to intelligent RFID and biometric access systems. By embedding real-time location sensors (RTLS) and RFID drug drawer tracking, hospital administrators can achieve 100% medication auditability, automated re-order triggers, and zero unauthorized narcotic access.
Legacy workstation trolleys relied on heavy lead-acid batteries with brief lifespans. Modern CE certified mobile carts incorporate ultra-lightweight Lithium Iron Phosphate (LiFePO4) power systems featuring intelligent battery management software (BMS), hot-swappable batteries, fast charging in under 2 hours, and over 3,000 charge cycles.
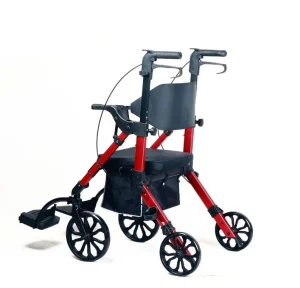
Hospital staff fatigue is a key driver of occupational injury. By combining high-strength extruded aluminum alloy framing with lightweight ABS components, modern delivery systems reduce pushing resistance by over 40%, ensuring effortless maneuverability through tight clinical hallways and elevator doors.
Comprehensive answers regarding CE certification, OEM/ODM customizations, quality assurance, and international logistics support.
All Shenzhen Avelar Medical workstation carts, emergency trolleys, and IV stands fully conform to European CE Medical Device Regulation (MDR 2017/745) requirements. Furthermore, our manufacturing facility operates strictly under ISO 13485:2016 quality management standards, and our electrical mobile computer carts meet IEC 60601-1 electrical safety and anti-static ESD standards.
Yes. With our in-house team of over 100 skilled engineers and complete manufacturing chain (laser cutting, CNC bending, robotic welding, powder spraying), we offer complete OEM/ODM capabilities. We can customize drawer configurations, color schemes, VESA mount height ranges, camera bracket attachments, and brand logos based on hospital tender blueprints.
For standard models, prototype samples can be shipped within 7 to 10 days. Standard containerized production orders (20ft/40ft HQ) typically take 25 to 35 business days from final technical drawing sign-off. We maintain strategic raw material stockpiles to accelerate urgent hospital emergency expansion orders.
We utilize high-grade medical electrostatically applied powder coatings that resist degradation from harsh clinical-grade disinfectants such as isopropyl alcohol, bleach, and hydrogen peroxide solutions. Non-porous surfaces, rounded corner radii, and seamless welds eliminate dirt traps and facilitate rapid wipe-down sanitation protocols.
We offer a comprehensive 3-to-5 year structural warranty across our cart frames and mechanical assemblies, along with 1-to-2 year warranties on electrical and battery components. We provide global distributors with replacement spare parts kits, video assembly guides, multi-language manuals, and 24/7 online technical engineering support.
Our carts utilize medical-grade, non-marking TPR/TPU dual-wheel casters featuring precision ball bearings, thread guards, and full 360-degree rotation. They are engineered for ultra-silent rolling (< 45 dB), anti-static grounding, and feature total-lock braking systems for absolute stability during stationary point-of-care operation.
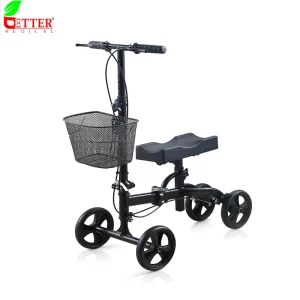
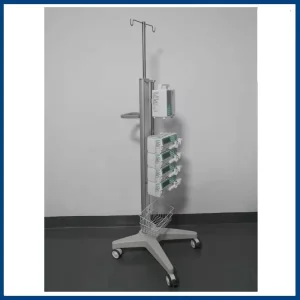
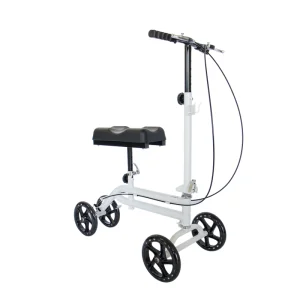
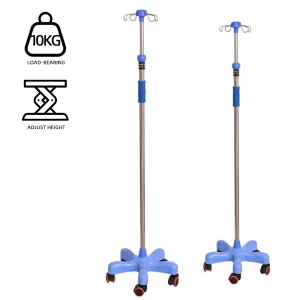
Explore our extended line of orthopedic knee scooters, difficult airway endoscopy carts, infusion drip stands, and specialty nursing trolleys.

 Avelar Medical