Top China Medical Support Solutions Supplier & Exporters

Engineered Hospital Furniture, Smart Mobile Nursing Carts, Ergonomic Patient Mobility Systems, and ISO13485-Certified Infrastructure for Global Healthcare Ecosystems

Clinical Equipment Showcase

Featured Mobile Medical Carts & Clinical Support Hardware

High-precision mobile workstations, emergency response carts, and infusion support solutions engineered to optimize hospital workflows and patient care safety.
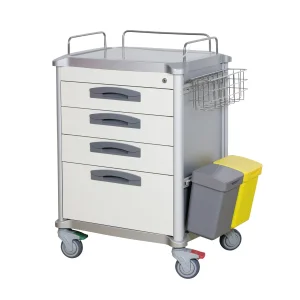
ABS Medium Capacity Hospital Medication Trolley Medical Drug Carts

ABS Medium Capacity Hospital Medication Trolley Medical Drug Carts

View Specifications →
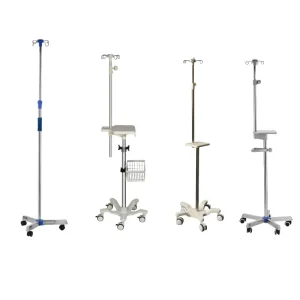
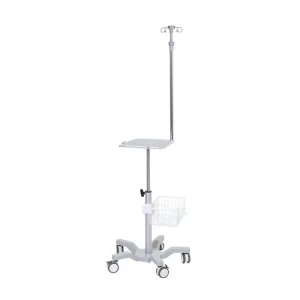
Infusion Stand with Height Adjustment Wheels Mobile IV Stand From Chinese Supplier Medical Use

Infusion Stand with Height Adjustment Wheels Mobile IV Stand From Chinese Supplier Medical Use

View Specifications →
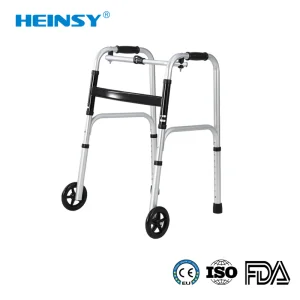
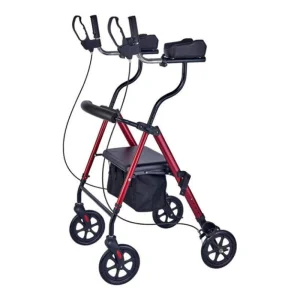
Hes-7102 Aluminum Alloy Promotion Custom Medical Seniors Elderly Upright Folding Frame Disabled Walking Aids Walker Rollator with Seat

Hes-7102 Aluminum Alloy Promotion Custom Medical Seniors Elderly Upright Folding Frame Disabled Walking Aids Walker Rollator with Seat

View Specifications →
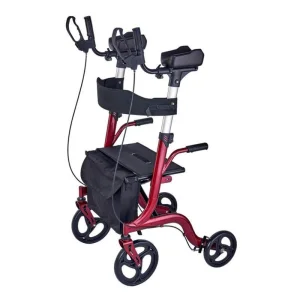
Wheel Drive Brother Medical or Customize Folding with Seat Upright Walker ISO

Wheel Drive Brother Medical or Customize Folding with Seat Upright Walker ISO

View Specifications →
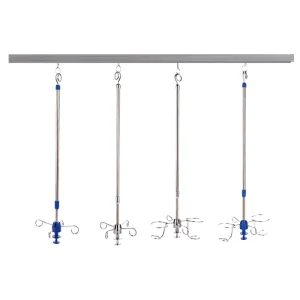
Hospital Medical Adjustable Mobile Infusion Stand/Bracket Infusion Rod Manufacturer

Hospital Medical Adjustable Mobile Infusion Stand/Bracket Infusion Rod Manufacturer

View Specifications →
Chenwei Cmw-303 CE Approved Anesthesia Workstation with Electronic Flow Meters

Chenwei Cmw-303 CE Approved Anesthesia Workstation with Electronic Flow Meters

View Specifications →
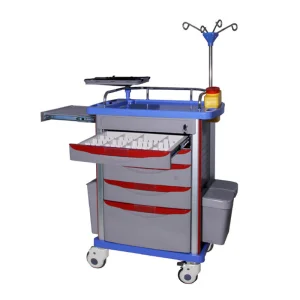
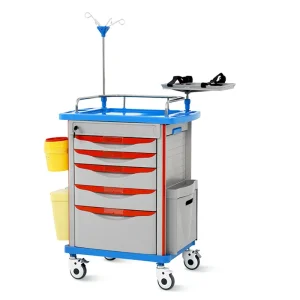
Medical ABS Emergency Ambulance Moving Nursing Crash Cart Trolley with 5 Drawers

Medical ABS Emergency Ambulance Moving Nursing Crash Cart Trolley with 5 Drawers

View Specifications →
Hospital Emergency Patients Medicine Dispensing Cart with Multiple Drawers

Hospital Emergency Patients Medicine Dispensing Cart with Multiple Drawers

View Specifications →
Industry Whitepaper & Clinical Insights

Global Landscape of Medical Support Solutions & Clinical Ecosystems

An authoritative strategic analysis on how modern hospital infrastructure, mobile workstation ergonomics, and patient mobility systems drive clinical workflow efficiency and infection control.

Shift Toward Ergonomic Mobile Workstations

Modern hospital environments demand seamless transition between acute treatment units, emergency rooms, and intensive care wards. Standardized mobile workstations reduce nursing fatigue, lower medication errors by up to 34%, and streamline electronic health record (EHR) integration right at the patient's bedside.

Infection Control & Polymer Engineering

Nosocomial infections remain a critical global healthcare challenge. China's leading medical support manufacturers utilize high-impact ABS thermoplastics, anti-bacterial powder coatings, and seamless stainless-steel welds that withstand aggressive hospital grade disinfectants (Isopropanol, Chlorine, Hydrogen Peroxide Vapors).

Rehabilitation & Demographic Trends

With global aging demographics intensifying across Europe, North America, and East Asia, demand for advanced upright posture walkers, bariatric commode handrails, and multi-functional rollators with modular seating has expanded at an estimated 8.4% CAGR, prioritizing structural integrity and user independence.

Key Industry Takeaway for Healthcare Buyers

Procuring medical support solutions directly from Tier-1 Chinese OEM/ODM suppliers provides overseas hospital networks, medical device distributors, and government health ministries with up to 45% capital expenditure savings without sacrificing ISO13485 quality standards, CE compliance, or structural durability.

Supply Chain Dominance

China Supply Chain Resilience & Manufacturing Synergy

Leveraging the Shenzhen-Huizhou hardware technology cluster to deliver world-class medical equipment manufacturing efficiency, high-volume agility, and absolute precision.

21+
Years Industry Mastery
10,000 m²
Production Infrastructure
100+
National Patents Secured
100+
Global Export Countries

Raw Material Hub Synergy

Situated in the heart of Greater Bay Area's industrial ecosystem, our facilities possess instant access to high-grade aviation aluminum alloys, surgical-grade 304/316 stainless steel, and medical-grade virgin ABS polymers with zero raw material lead-time delays.

200+ Advanced Machinery Units

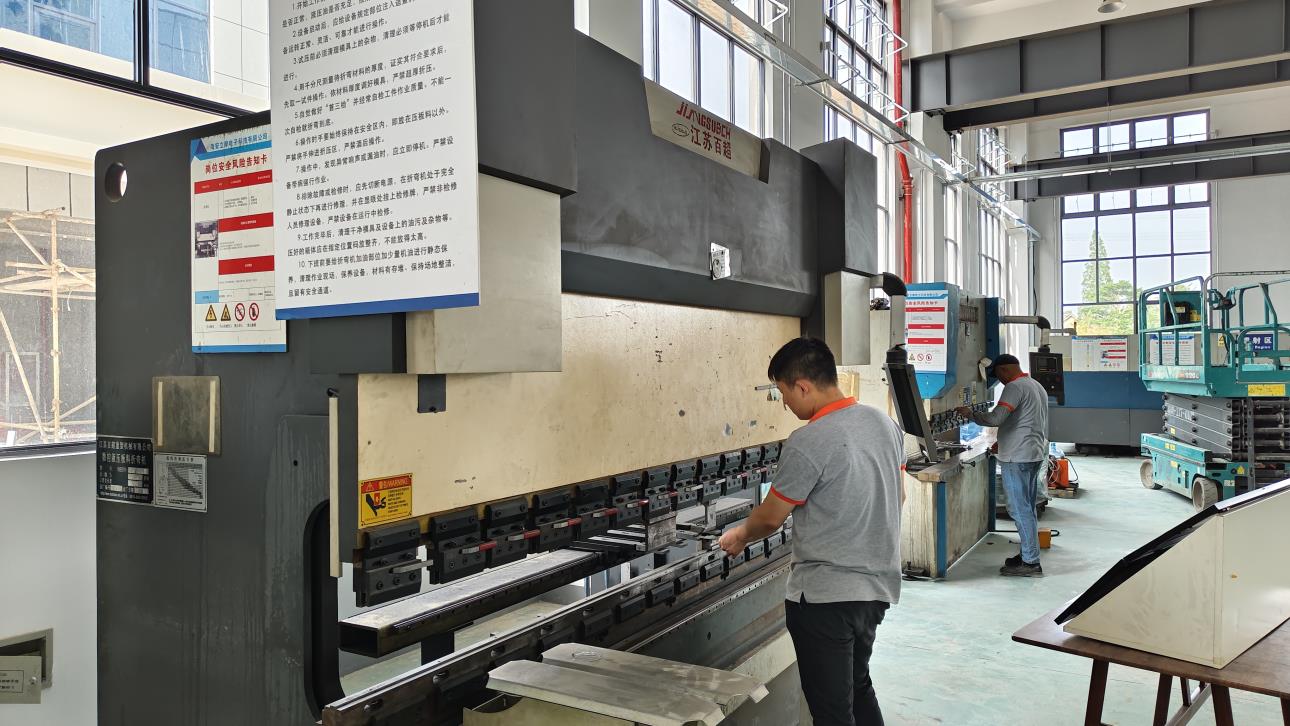
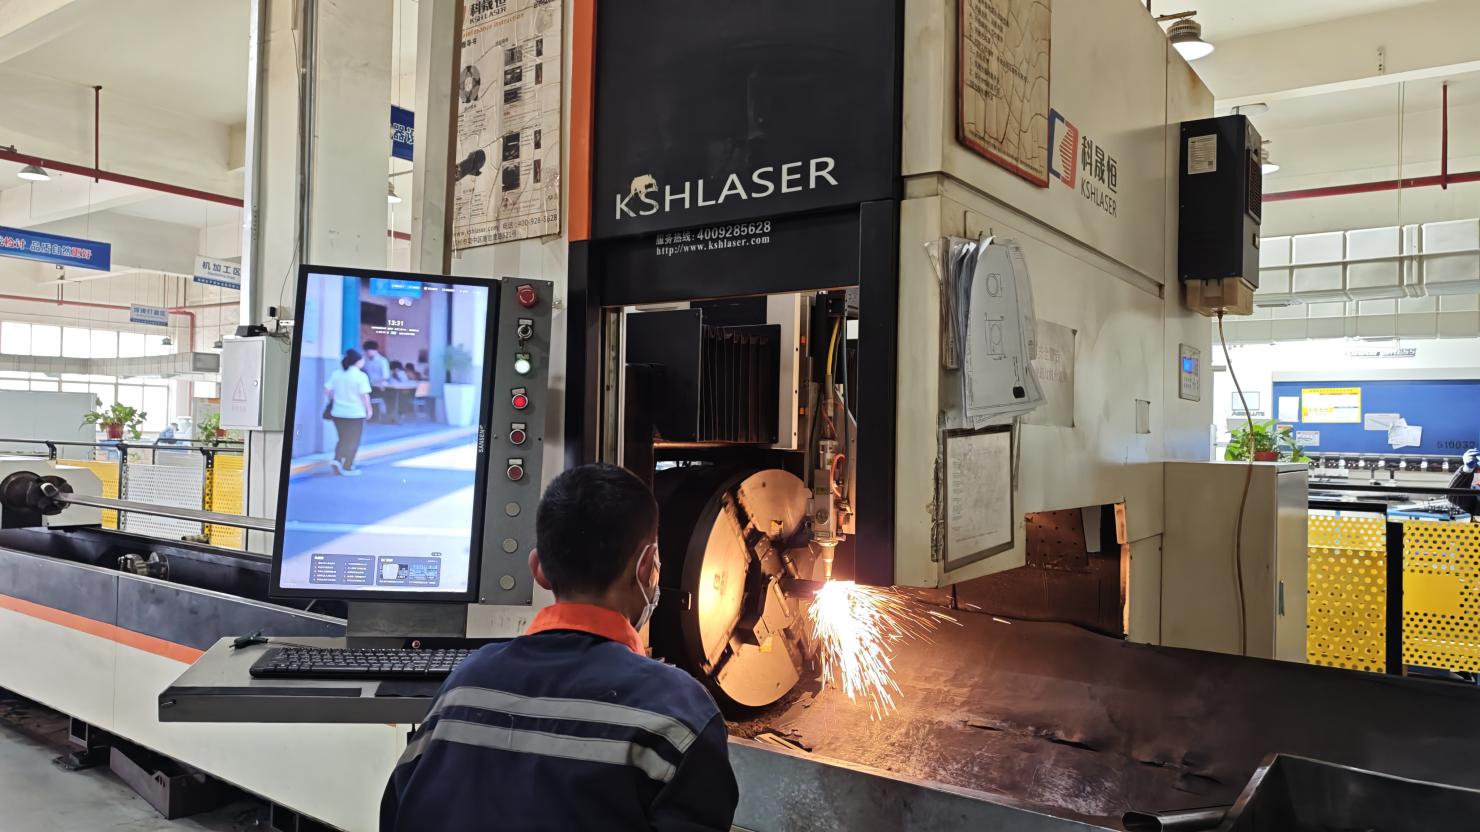
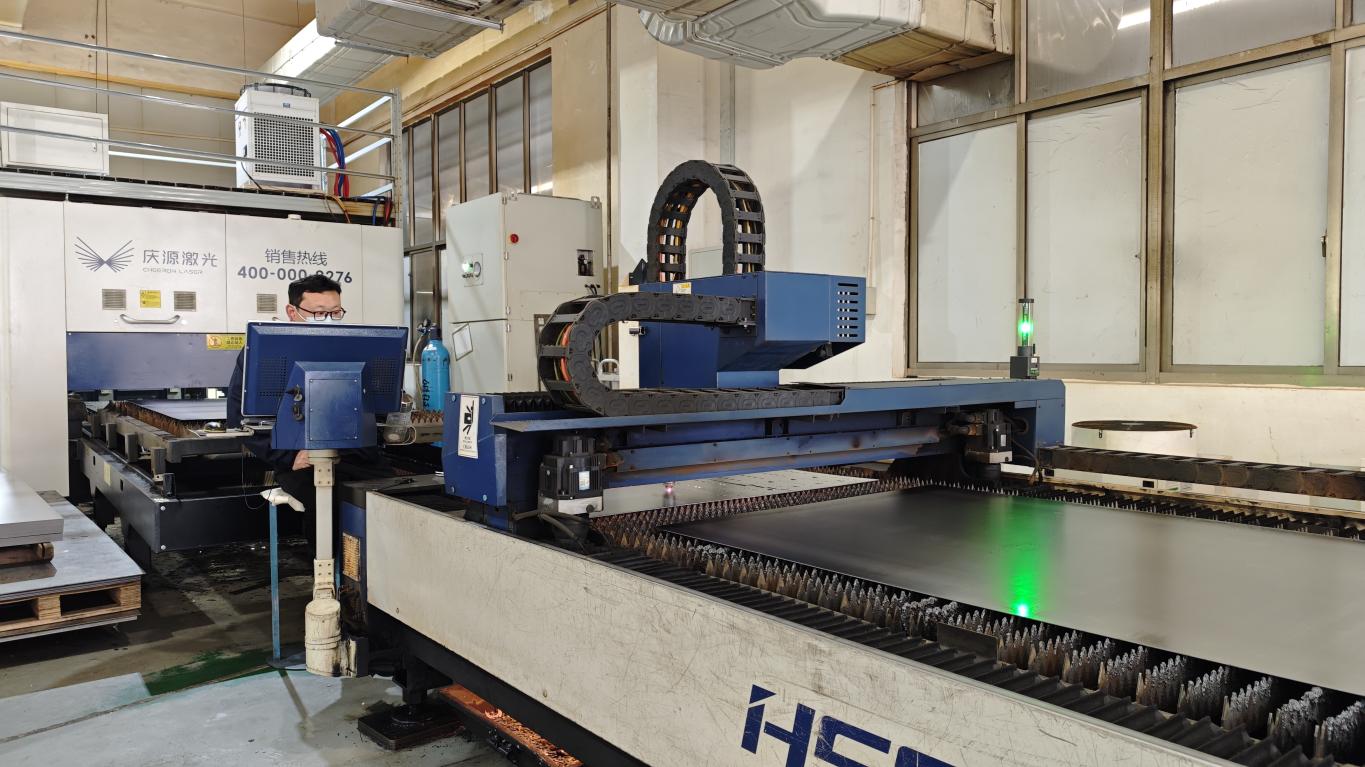
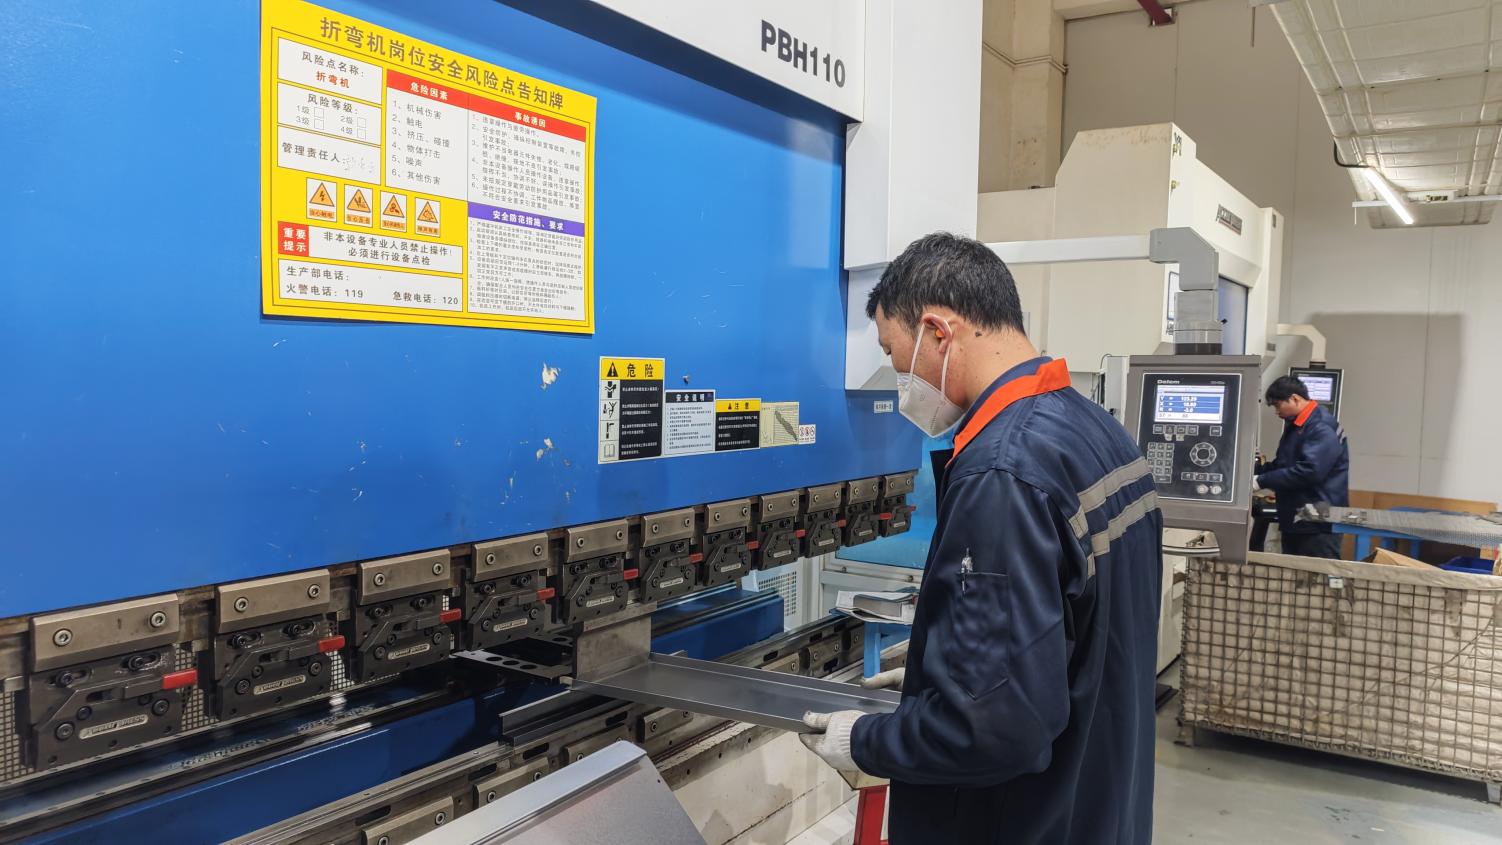
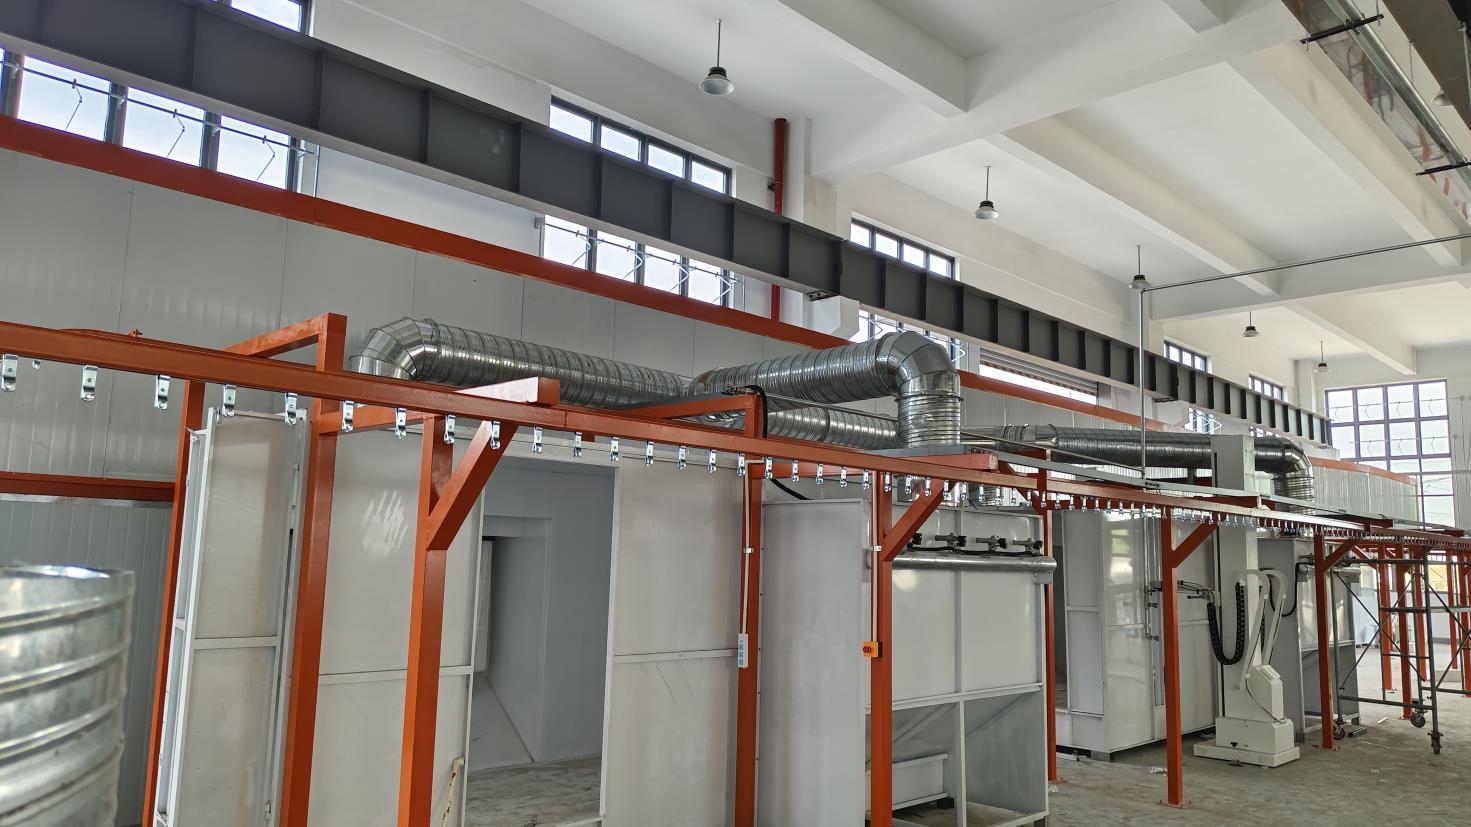
Equipped with high-precision fiber laser cutting systems, multi-axis CNC bending machines, automated robotic welding cells, and electrostatic powder coating lines to maintain structural tolerances within micro-millimeters.

Robust Logistics Resilience

Direct proximity to Yantian and Shekou deep-water ports allows frictionless container shipping, flexible FOB/CIF/DDP arrangements, and emergency air-freight dispatch capabilities for urgent pandemic response or hospital expansion contracts.

Quality Assurance Flow

State-of-the-Art Precision Manufacturing Pipeline

Every component of our medical support solutions undergoes rigorous multi-stage fabrication, automated machining, and strict quality verification to guarantee field reliability.
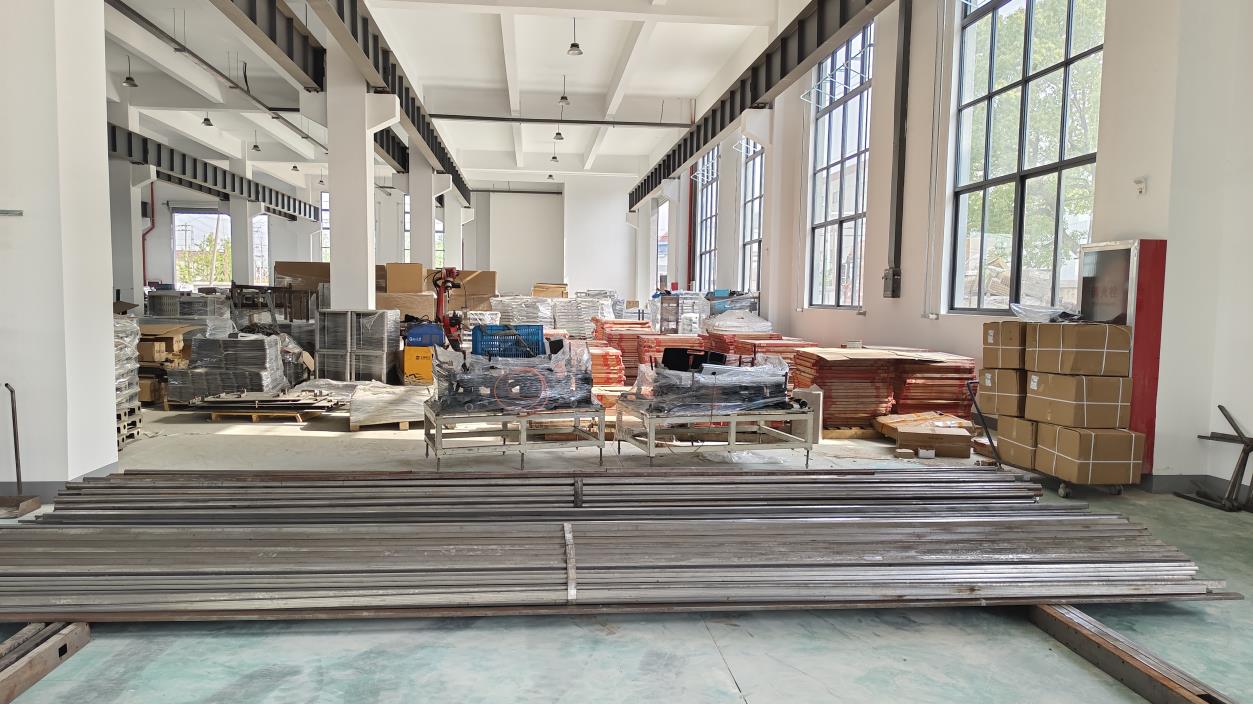
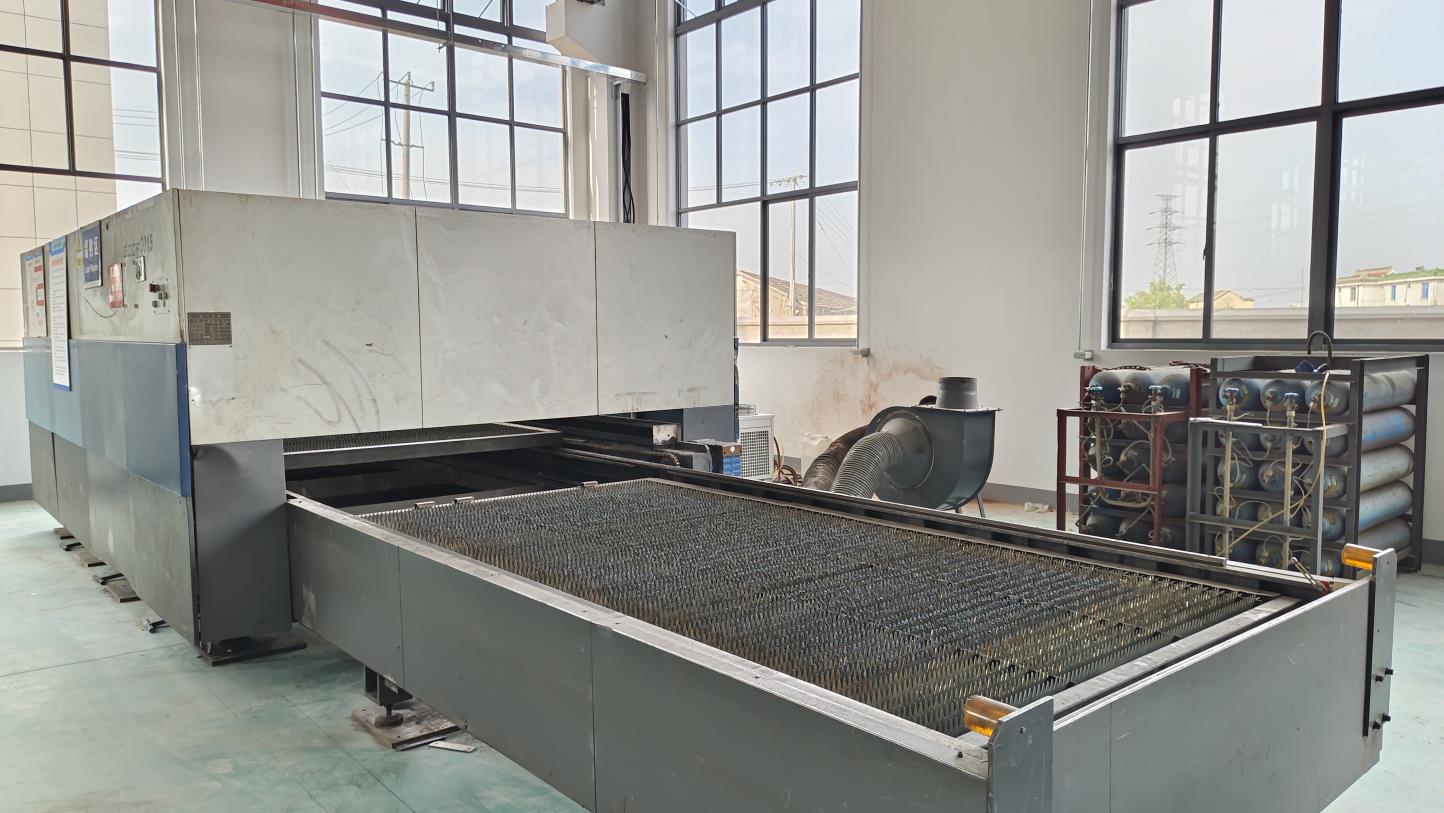
Raw Material Inspection
1. Raw Material Selection
Laser Cutting Process
2. High-Precision Laser Cutting
Shearing Operation
3. Metal Sheet Shearing
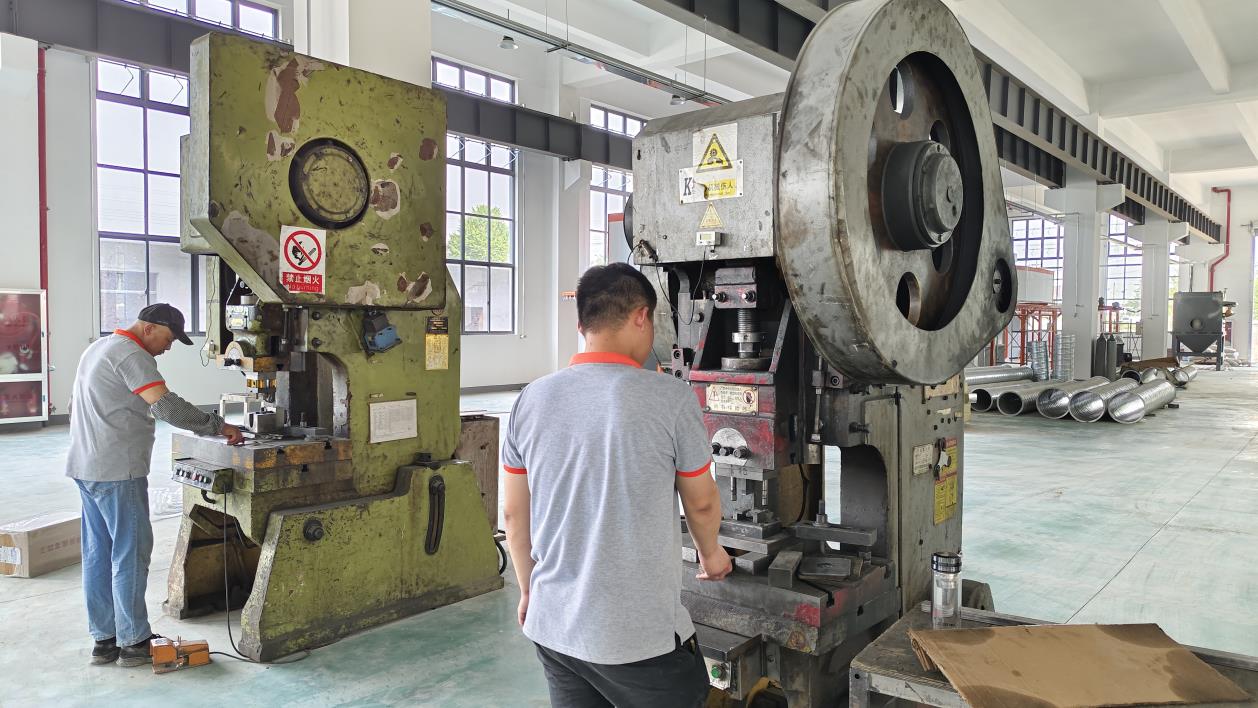
Punching Station
4. Automated Punching
Tube Cutting
5. Structural Tube Cutting
Plate Cutting
6. Heavy Plate Cutting
CNC Bending
7. CNC Sheet & Tube Bending
Robotic Welding
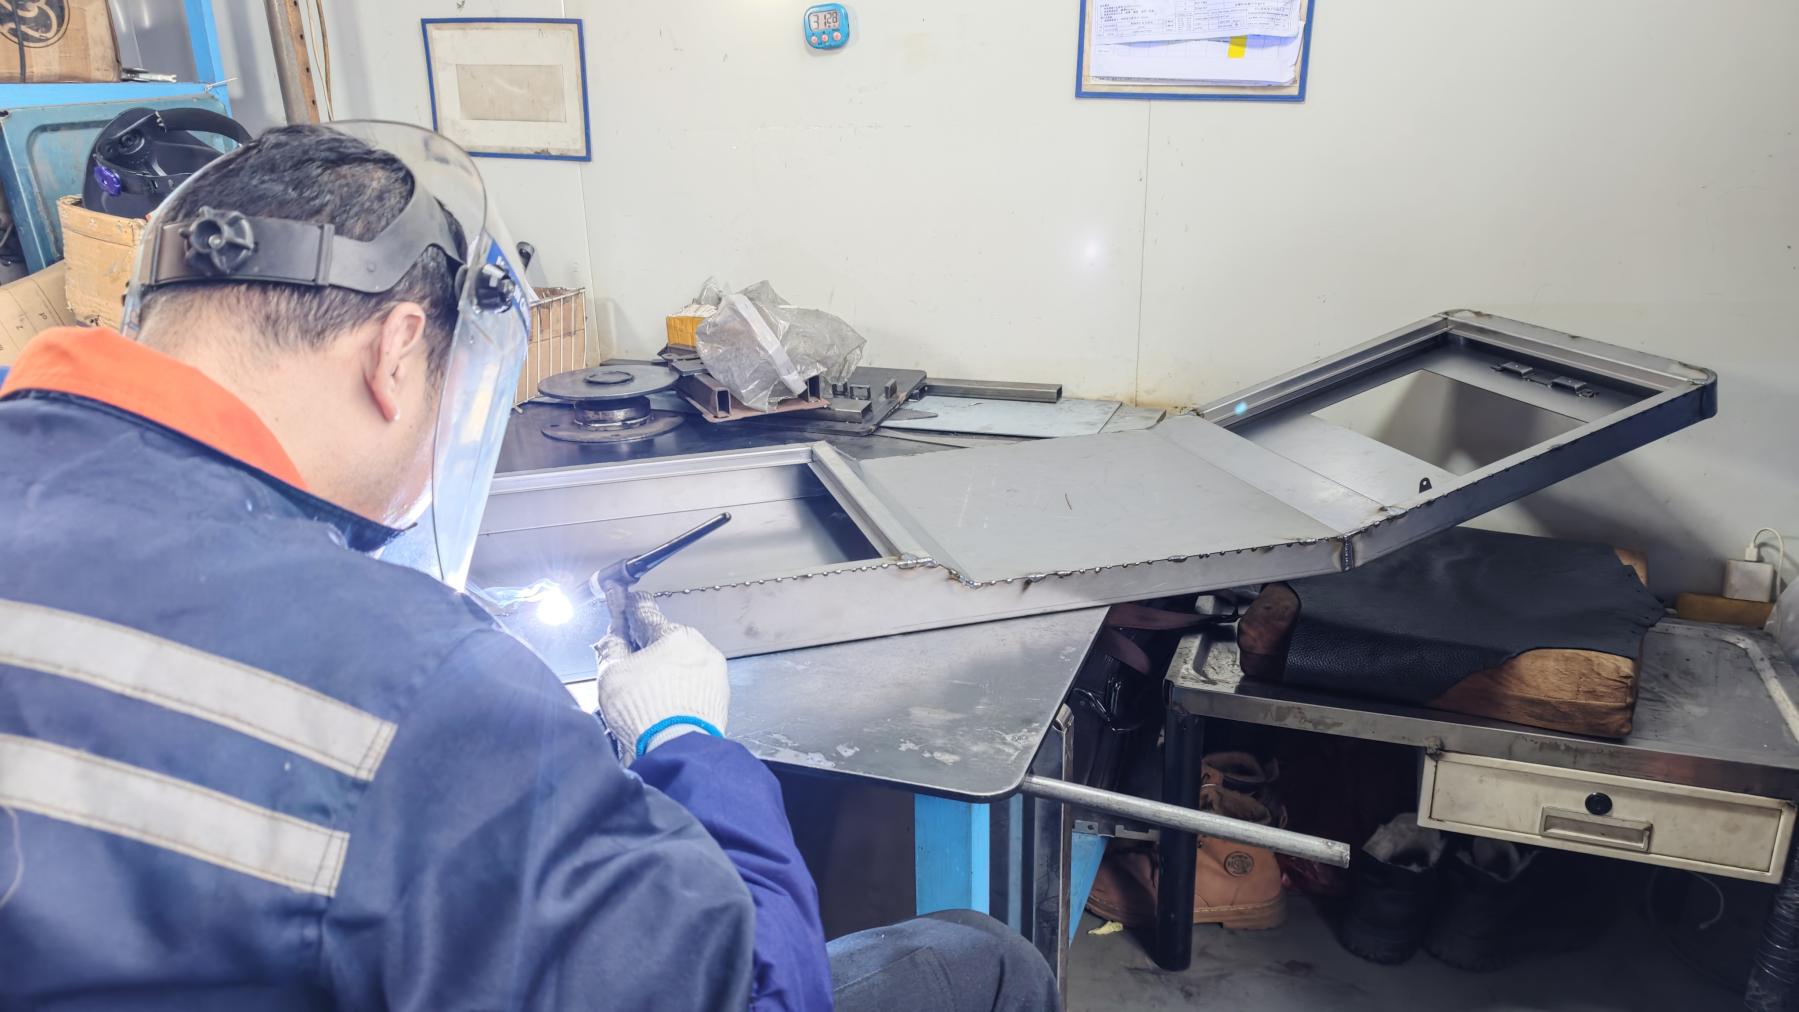
8. Robotic & TIG Welding
Surface Polishing
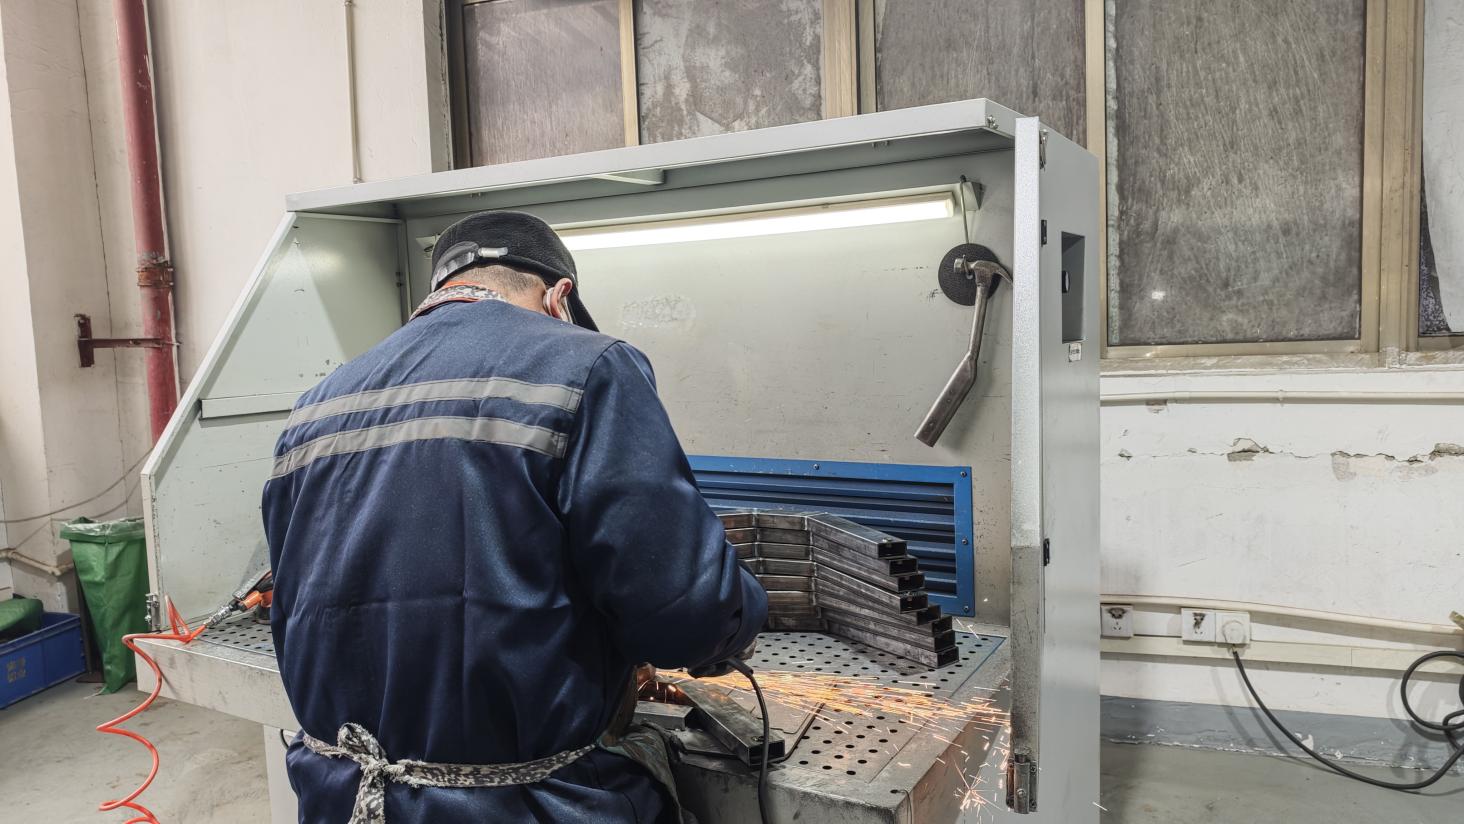
9. Seamless Surface Polishing
Electrostatic Spray Painting
10. Electrostatic Powder Coating
Precision Assembly
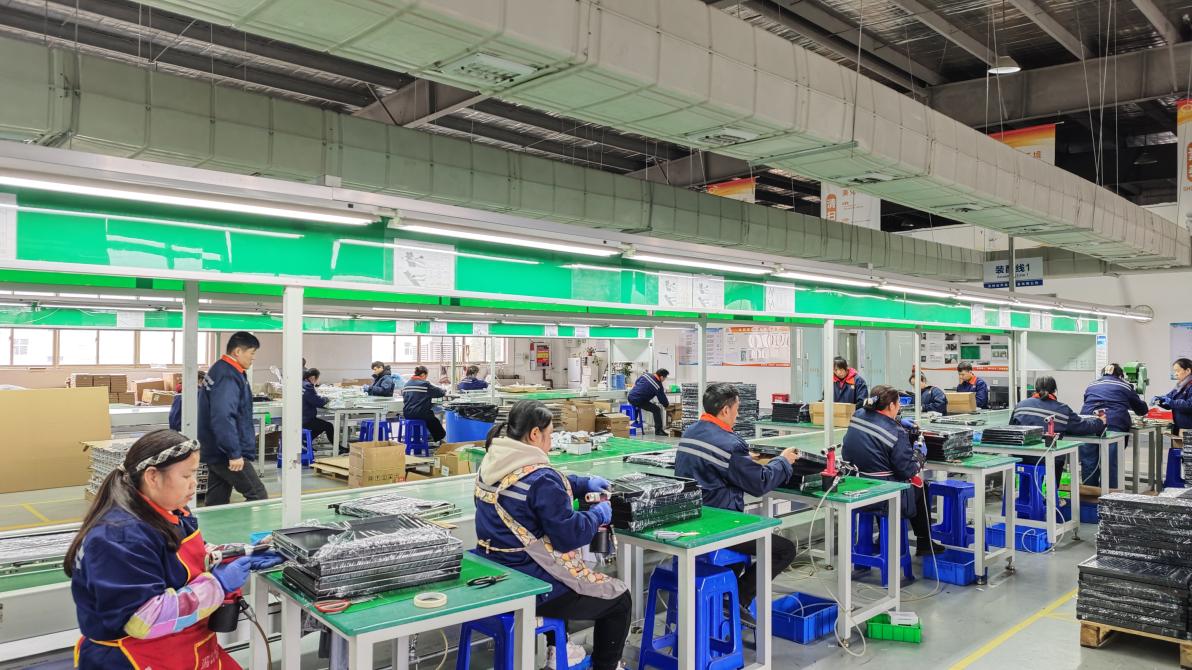
11. Modular Component Assembly
Laser Marking
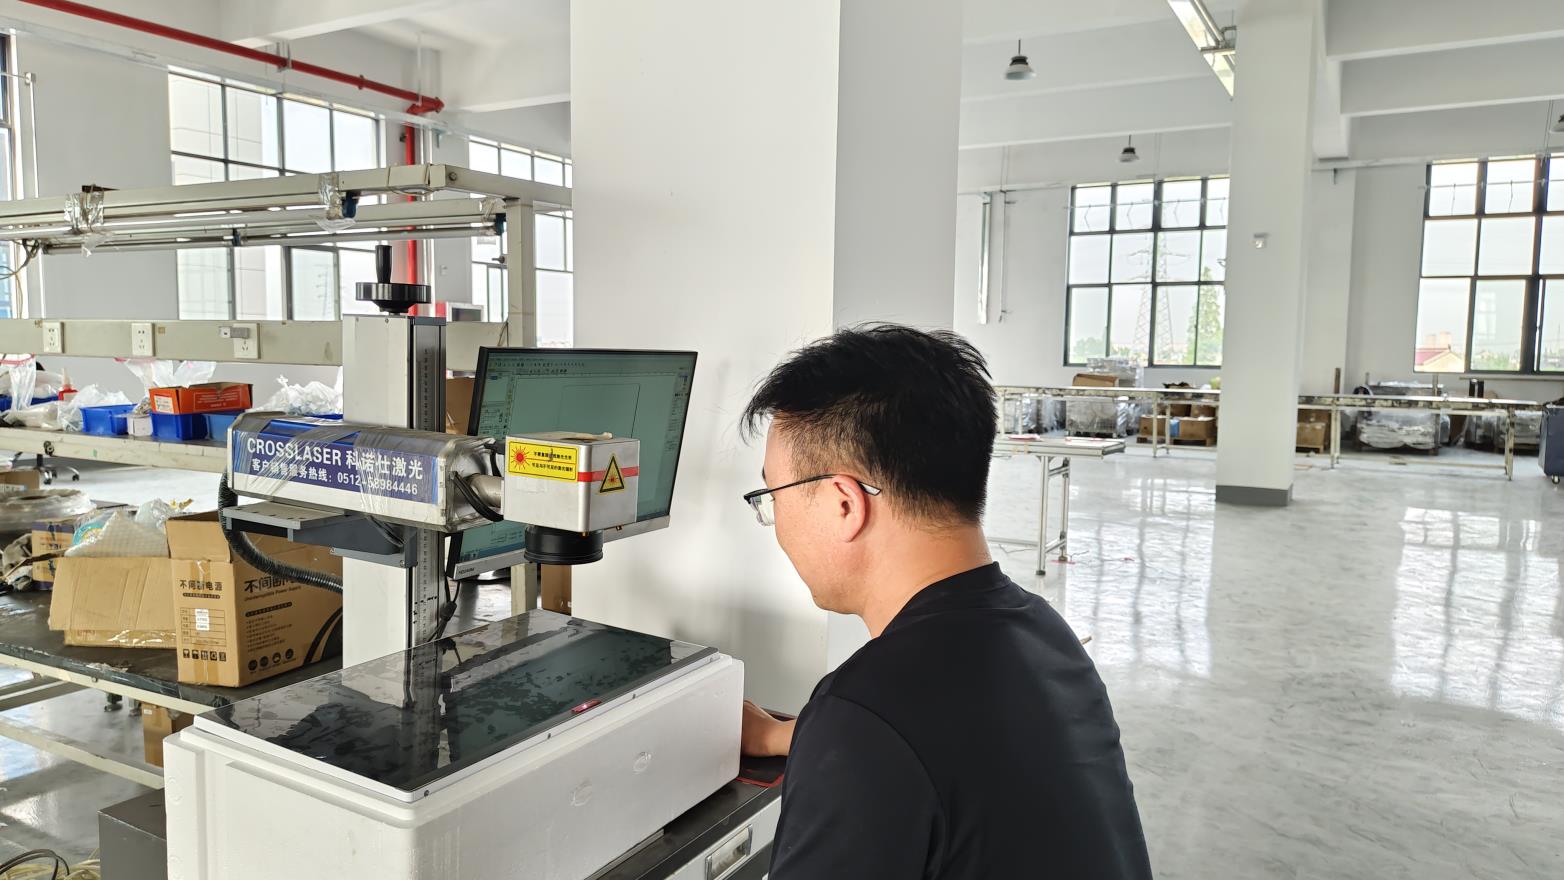
12. UDI Laser Marking & Traceability
Final Quality Check
13. Final Calibration & Testing
Export Packaging
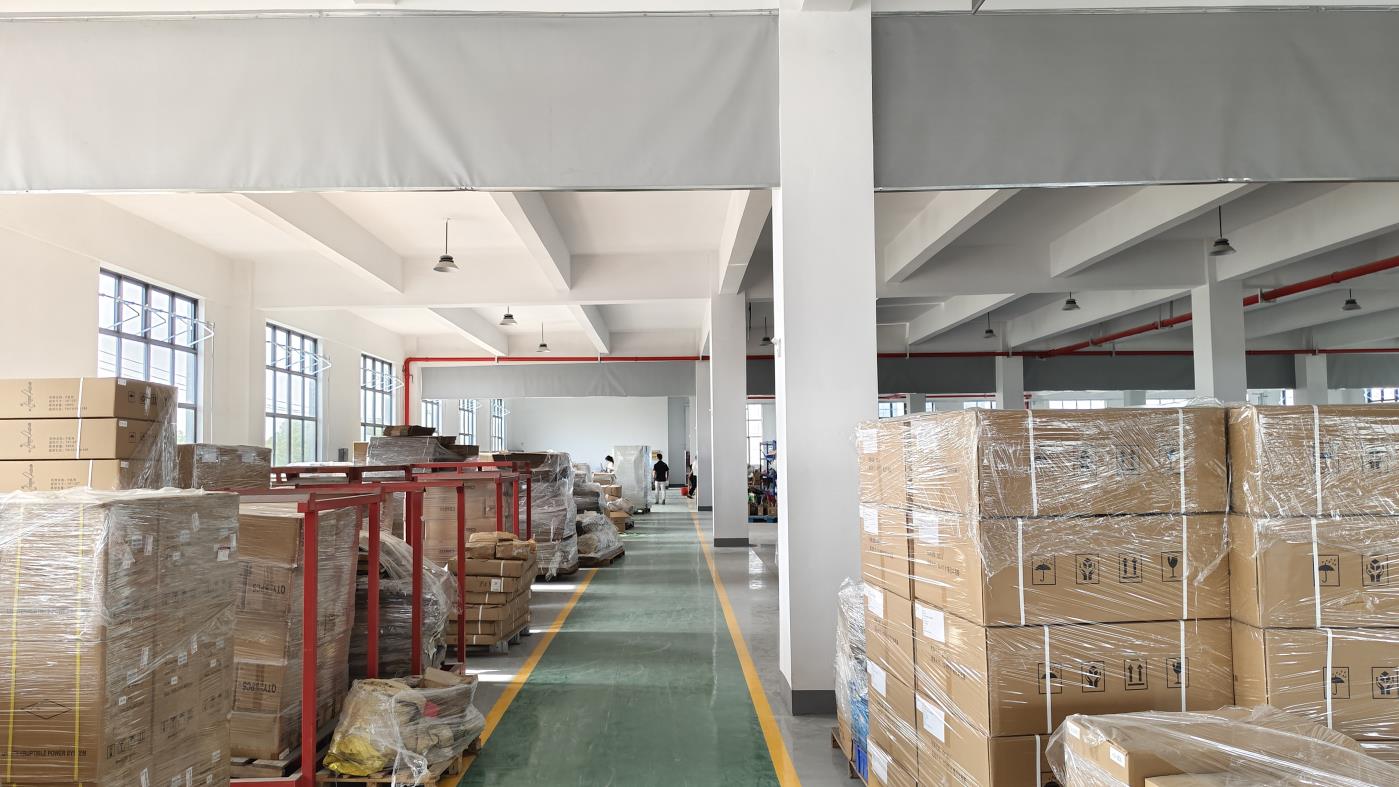
14. Shockproof Export Packaging
Clinical Versatility

Localized Application Scenarios in Modern Healthcare Systems

Tailored support hardware configured for emergency response, acute ward treatment, surgical theaters, and home care environments.

Intensive Care Units (ICU) & Emergency Rooms (ER)

During critical resuscitation or acute trauma management, seconds count. Our emergency crash carts feature centralized break-away locks, multi-layer drawer organizers, oxygen cylinder holders, and built-in CPR boards. Integrated heavy-duty silent casters enable smooth 360-degree maneuverability across carpeted or epoxy floorings without disruptive noise.

Operating Theaters & Anesthesia Stations

Precision anesthesia workstations require stable structural mounting, continuous power distribution, and anti-static construction. Our workstations support multi-parameter monitoring, electronic flow meters, and vaporizers, maintaining seamless interaction between surgical teams, anesthesiologists, and life support monitoring systems.

Outpatient Infusion & Routine Ward Dispensing

For high-volume day-clinics and ward rounds, height-adjustable mobile IV poles with weighted cast-iron bases prevent tip-overs during rapid patient transport. ABS medication trolleys feature customizable bin dividers, smooth sliding drawer tracks, and keycard/combination locks to safeguard narcotics and controlled pharmaceuticals.

Geriatric Rehabilitation & Bariatric Patient Support

Designed for post-operative recovery, eldercare facilities, and bariatric care units. Forearm support posture walkers relieve wrist stress while promoting upright spinal alignment. Heavy-duty stainless steel grab bars and reinforced commode handrails deliver structural loads up to 250kg, ensuring patient dignity and safety.

R&D Vision

Technological Roadmap & Next-Gen Smart Hardware

Integrating IoT intelligence, lightweight material science, and predictive ergonomics into the next generation of clinical support devices.

IoT Asset Tracking & Smart Locking

Incorporating RFID and BLE (Bluetooth Low Energy) tracking sensors into medication and crash carts allows real-time hospital asset localization, automated inventory auditing, and electronic audit-trail access control to reduce drug shrinkage and asset misplacement.

Motorized Kinematics & Power Assist

Developing lithium-powered electric drive assistance for heavy-duty emergency carts and bariatric transport chairs, enabling single-nurse operation on inclines, long corridors, and high-load emergency transfers without physical strain.

Nanotechnology Anti-Microbial Surfaces

Formulating silver-ion and titanium dioxide nanoparticle additive coatings into molded polymer surfaces to actively suppress 99.9% of bacterial growth (Staphylococcus aureus, E. coli) over the operational lifetime of the medical furniture.

Compliance & Assurance

Global Regulatory Compliance & Localized Support

Fulfilling stringent international healthcare standards and guaranteeing continuous post-sale technical operations worldwide.

International Certification Matrix

Navigating global regulatory landscapes requires absolute adherence to quality management protocols. Our manufacturing facilities operate under comprehensive ISO13485:2016 Quality Management Systems for Medical Devices.

  • CE Mark (EU MDR Compliance): Complete technical documentation and safety compliance for European Union healthcare procurement.
  • FDA Registered Facilities: Strict alignment with US Food and Drug Administration manufacturing practice regulations.
  • RoHS & REACH Certified Polymers: Non-toxic, heavy-metal-free, and environmentally sustainable materials across all plastic components.
  • Biocompatibility & Structural Load Testing: Rigorous static load, dynamic caster durability, and flame-retardant evaluations.

Global Customer Support Guarantee

We extend far beyond standard manufacturing by offering dedicated technical assistance for international medical project bids and hospital supply contracts:

✔ 2-Year Comprehensive Structural Warranty
✔ Modular Spare Parts Dispatch within 48 Hours
✔ Custom OEM/ODM Engineering Drawing Support in CAD/3D STEP
✔ Multilingual Technical Documentation & Assembly Manuals

About The Enterprise

Who We Are — Shenzhen Avelar Medical Co., Ltd.

21+ years of pioneering innovation, precision engineering, and dedicated service in global healthcare support solutions.

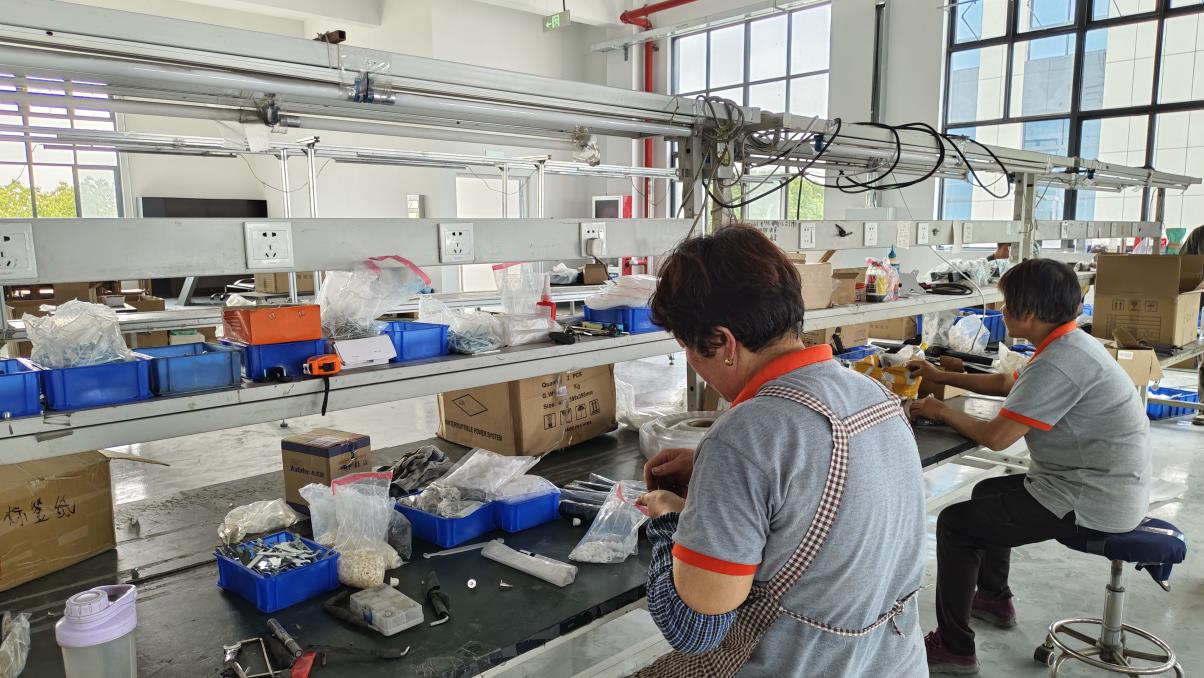
Shenzhen Avelar Medical Co., Ltd. was founded in 2003 and has accumulated over 21 years of rich experience in the medical technology industry. Headquartered in Pingshan, Shenzhen, with a state-of-the-art production facility in Huizhou, the company spans a total area of 10,000 square meters. As a leading national high-tech enterprise, Avelar Medical integrates cutting-edge research and development, innovative design, and high-efficiency manufacturing to deliver superior medical and healthcare solutions.

With a team of over 100 highly skilled engineers and technical professionals, and more than 200 advanced manufacturing units, Avelar Medical is committed to pushing the boundaries of technological advancements in the medical field. The company has secured more than 100 national patents, demonstrating our continuous focus on innovation.
Shenzhen Avelar Medical Facility

Avelar Medical specializes in a broad range of products, including medical equipment installation solutions, intelligent mobile medical devices, assistive technology for residual life support, healthcare products for the bathroom, and more. We work closely with top-tier hospitals and healthcare institutions around the world, providing them with products designed to improve patient care, enhance operational efficiency, and optimize the healthcare environment. Our solutions have reached more than 100 countries and regions, including North America, Europe, the Middle East, and Asia.

At Shenzhen Avelar Medical, our business philosophy revolves around two core principles: “Quality First” and “Customer First.” This commitment to excellence has earned us the trust of our domestic and international clients. Our innovative products, combined with exceptional service and reliable after-sales support, allow us to meet the ever-evolving needs of the global healthcare market.

As we look to the future, Avelar Medical remains dedicated to continuous growth, investment in research and development, and the creation of cutting-edge medical solutions. We are committed to improving healthcare outcomes, fostering a healthier future for communities worldwide, and making a lasting impact on the global healthcare industry.
Avelar Medical Factory Production Floor
Extended Product Portfolio

Specialized Diagnostic Carts & Patient Assistive Mobility Devices

Explore our full line of endoscopy carts, ECG roll stands, patient posture walkers, and bariatric bathroom grab rails.
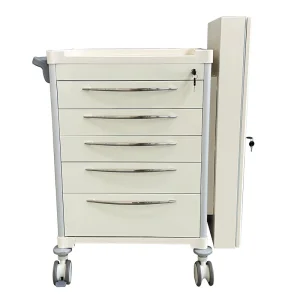
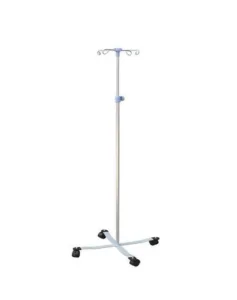
High Strength Removable Hospital Clinic Patient Difficult Airway Endoscopy Trolleys

High Strength Removable Hospital Clinic Patient Difficult Airway Endoscopy Trolleys

View Specifications →
Hospital Mobile Stainless Steel Infusion IV Pole Drip Stand

Hospital Mobile Stainless Steel Infusion IV Pole Drip Stand

View Specifications →
Portable Forearm Support Upright Walker Folding Seat Posture Walker

Portable Forearm Support Upright Walker Folding Seat Posture Walker

View Specifications →
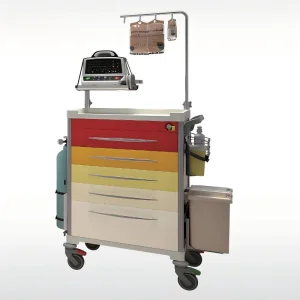
Nwm054-Et FDA Multi-Function Hospital Nursing Furniture Emergency Medical Crash Cart

Nwm054-Et FDA Multi-Function Hospital Nursing Furniture Emergency Medical Crash Cart

View Specifications →
Elderly Stand up Rollator Forearm Support Walker with Seat

Elderly Stand up Rollator Forearm Support Walker with Seat

View Specifications →
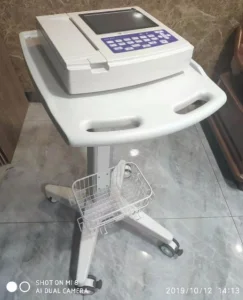
CE RoHS Passed Medical Roll Stand Carts for ECG

CE RoHS Passed Medical Roll Stand Carts for ECG

View Specifications →
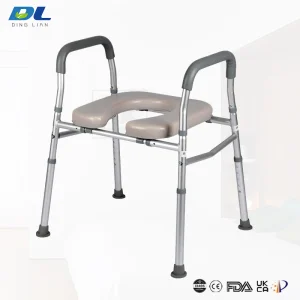
Dinglian Dl-2016la High Strength Commode Handrail for Bariatric Patients Heavy Duty Toilet Grab Bars

Dinglian Dl-2016la High Strength Commode Handrail for Bariatric Patients Heavy Duty Toilet Grab Bars

View Specifications →
Aluminum Alloy Mobile Infusion Stand with Height-Adjustable Infusion Tube Holder

Aluminum Alloy Mobile Infusion Stand with Height-Adjustable Infusion Tube Holder

View Specifications →
Knowledge Base & FAQ

Frequently Asked Questions by Global Medical Procurement Officers

Detailed technical and commercial answers regarding medical support equipment sourcing, customization, certifications, and logistics.

1. Why source Medical Support Solutions & Hospital Carts directly from China manufacturers like Avelar Medical?
Sourcing directly from established Chinese medical manufacturers like Shenzhen Avelar Medical Co., Ltd. provides profound cost advantages (typically 30%-50% savings over European or North American distributors) without compromising quality. With 21+ years of engineering mastery, 10,000 m² of certified manufacturing space, and full control over laser cutting, CNC bending, and powder coating, Avelar delivers ISO13485 and CE compliant medical carts and mobility solutions tailored precisely to global hospital tender specifications.
2. Can Avelar Medical accommodate custom OEM/ODM modifications for specialized clinical Carts?
Yes. Supported by a dedicated R&D engineering team of over 100 professionals and holding more than 100 national patents, Avelar Medical specializes in OEM/ODM customization. We can modify physical dimensions, drawer configurations, caster specifications, locking mechanisms (centralized keyless, electronic keypad, RFID), color palettes, laser-etched branding, and specialized mounting arms for medical monitors or ECG devices.
3. What international certifications do Avelar Medical support products hold?
Our medical equipment installation solutions, mobile carts, anesthesia workstations, and patient walking aids comply with major international regulatory frameworks. We hold ISO13485 certification for medical device quality management, CE mark approval under European Medical Device Regulations (MDR), FDA registration for US hospital imports, and RoHS/REACH chemical safety compliance for all polymer materials.
4. How does Avelar ensure long-term durability and infection control on medical carts?
We use high-impact ABS thermoplastic panels, aviation-grade anodized aluminum pillars, and 304 stainless steel framework. All steel surfaces undergo multi-stage automatic electrostatic powder coating with antimicrobial additives. The seamless joint engineering eliminates hard-to-clean crevices, preventing bacterial accumulation and allowing thorough cleaning with harsh medical-grade chemical disinfectants.
5. What is the typical lead time and packaging quality for international bulk shipments?
Standard product orders are typically manufactured and dispatched within 15 to 25 business days. Custom OEM/ODM batches range from 30 to 45 days depending on tooling requirements. Every medical cart and mobility device is packaged in heavy-duty export honeycomb cartons or reinforced wooden crates lined with high-density shock-absorbing EPE foam, tested according to ISTA transit standards to guarantee damage-free sea or air freight delivery.